Double Wall Cup

DAILYECO, Your Professional Double Wall Paper Cup Manufacturer

Custom Double Wall Paper Cup for Hot Beverage Packaging

Key Facts About Double Wall Paper Cup

Item

Information

Product Name

Double Wall Paper Cup

Material

Food-Grade Paperboard

Product Type

Double Wall Hot Beverage Cup

Typical Sizes

4oz, 6oz, 8oz, 10oz, 12oz, 16oz, 20oz,22oz

Applications

Coffee Shops, Cafés, Restaurants, Hotels, Offices, Catering, Events

Beverage Types

Coffee, Tea, Latte, Cappuccino, Espresso, Hot Chocolate

Wall Structure

Double Wall Insulated Construction

Coating Options

PE, PLA, Water-Based Barrier

Customization

OEM & ODM Available

Printing

CMYK, Pantone, Full Surface Printing

Compatible Lids

Paper Lid, PP Lid, PS Lid, Sip Lid

Supply Type

Manufacturer & Supply Chain Partner

Export Markets

North America, Europe, Australia, Middle East, Asia


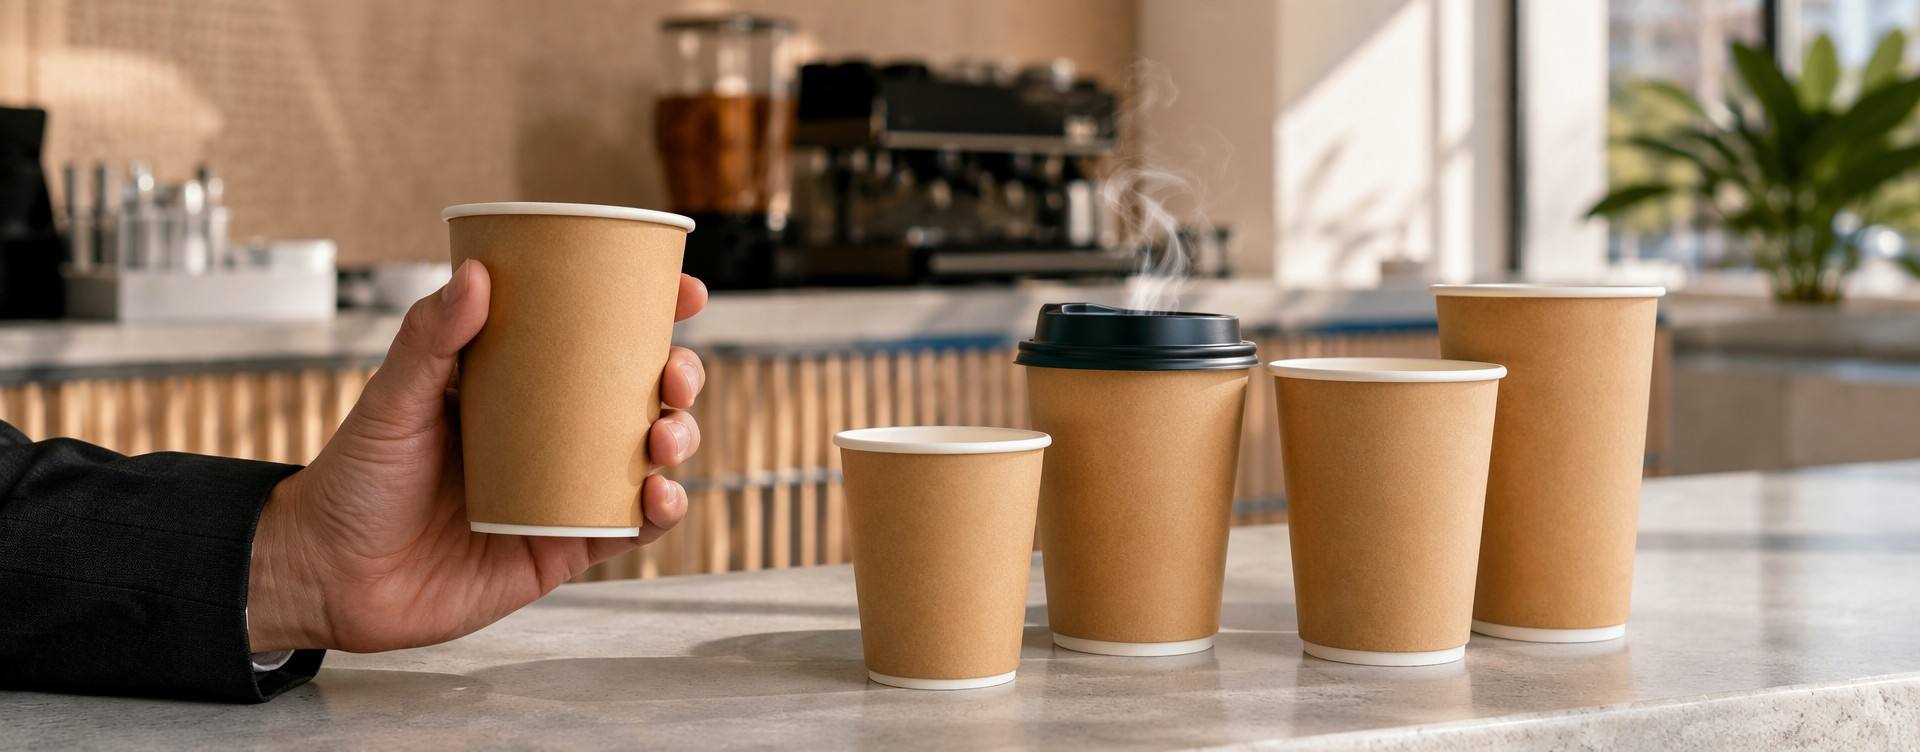
Double wall paper cups are insulated disposable beverage cups manufactured with two layers of food-grade paperboard. The additional outer wall creates an insulating air gap that improves heat retention while keeping the outer surface comfortable to hold, eliminating the need for separate paper sleeves in many hot beverage applications.

Compared with traditional single wall paper cups, double wall paper cups offer enhanced thermal insulation, improved rigidity, and a larger printable surface for premium branding. They are widely used by coffee shops, cafés, quick-service restaurants, foodservice distributors, hospitality groups, and takeaway beverage brands seeking a professional and comfortable drinking experience.

DAILYECO supplies both self-manufactured and supply-chain-supported double wall paper cup solutions, including OEM production, private-label branding, custom printing, and global export services for professional B2B customers.


What Are Double Wall Paper Cups? 

Double wall paper cups are disposable hot beverage containers engineered with two separate layers of paperboard. Unlike standard single wall paper cups, the additional outer layer creates a pocket of insulating air between the inner and outer walls, helping reduce heat transfer while maintaining beverage temperature.

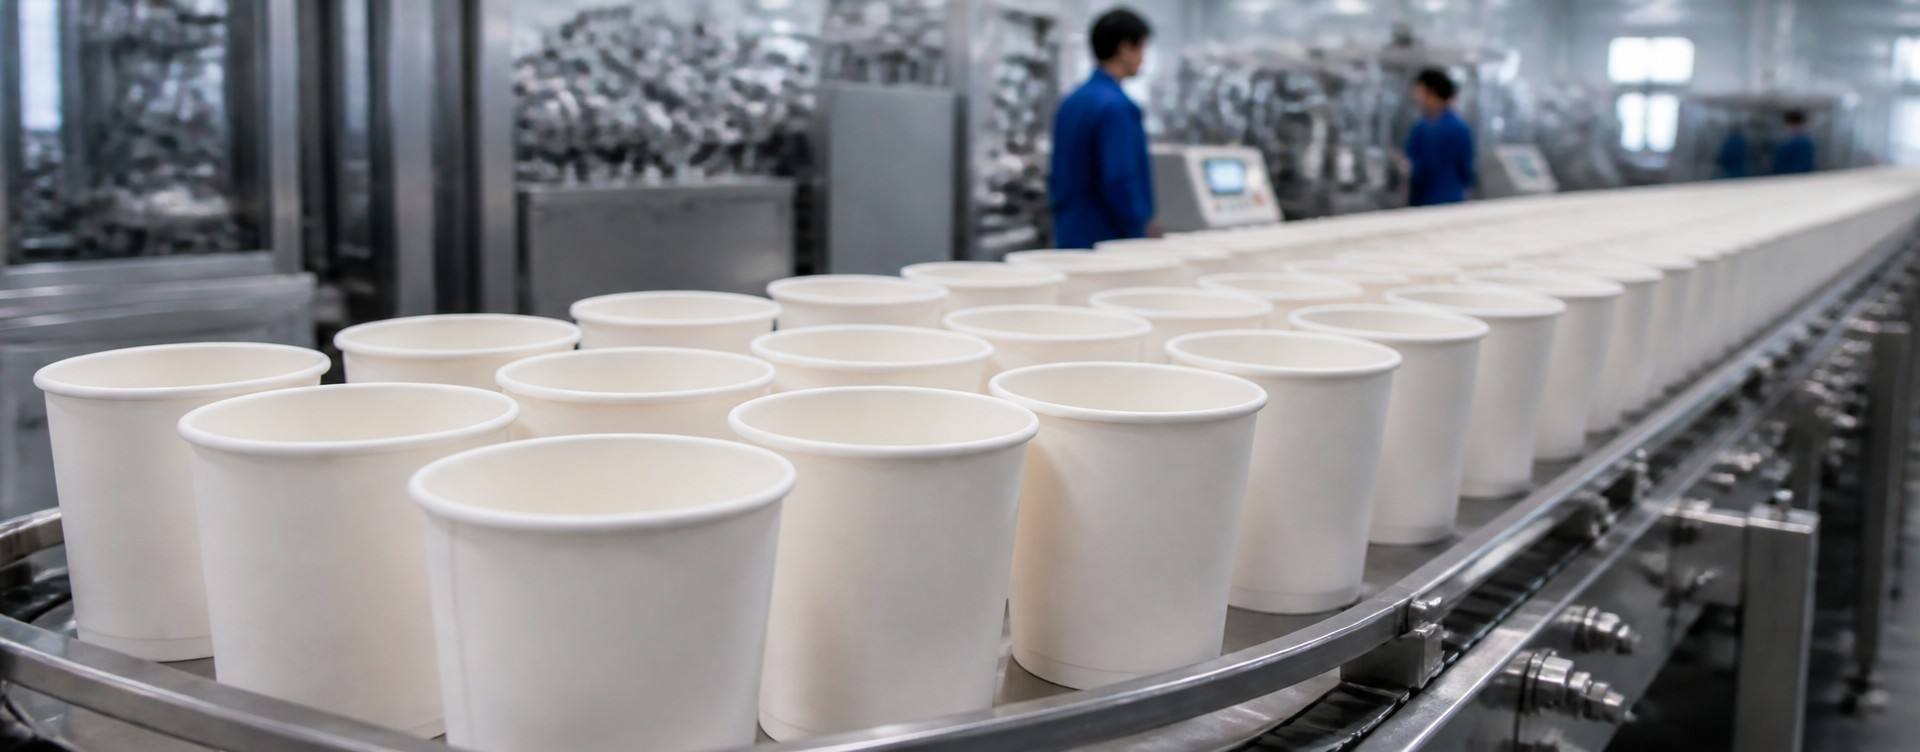
The manufacturing process begins with high-quality food-grade paperboard, which is formed into an inner cup before being wrapped with a second outer paper layer. Depending on customer requirements and target market regulations, the inner cup may be produced with PE coating, PLA coating, or emerging water-based barrier technologies to improve liquid resistance.

Because the insulating layer reduces heat transfer, customers can comfortably hold hot drinks without requiring an additional sleeve in many applications. At the same time, the larger outer surface provides an excellent canvas for high-quality branding, making double wall paper cups a preferred packaging solution for premium coffee shops and beverage chains.

Today, double wall paper cups are widely used for takeaway coffee, specialty beverages, tea service, corporate catering, hotel breakfast programs, convenience stores, and food delivery operations. Their combination of insulation performance, attractive appearance, and customization flexibility has made them one of the fastest-growing categories in the disposable beverage packaging industry.

For businesses looking to improve customer experience while strengthening brand presentation, double wall paper cups provide a practical, scalable, and commercially proven packaging solution.


What Are the Key Features of Double Wall Paper Cups? 

Feature

Performance

Explanation

Double Wall Construction

Excellent

Creates an insulating air layer between two paper walls

Heat Insulation

Excellent

Keeps beverages warmer while reducing surface heat

Comfortable Grip

Excellent

Often eliminates the need for paper sleeves

Structural Strength

Excellent

Increased rigidity compared with single wall cups

Printing Performance

Excellent

Larger printable surface for premium branding

Food Contact Safety

Food Grade

Manufactured using food-contact compliant materials

Leak Resistance

Excellent

Reliable performance for hot beverages

Custom Branding

Available

OEM printing and private-label packaging

Lid Compatibility

Excellent

Compatible with paper, PP, and PS lids

Sustainability Options

Available

PE, PLA, and water-based coating options

The primary advantage of double wall paper cups is their ability to combine thermal insulation, premium appearance, and branding opportunities within a single packaging solution. They enhance customer comfort while supporting stronger brand visibility for coffee shops and foodservice businesses.
Double Wall Paper Cup Structure and Thermal Insulation


Why Are Double Wall Paper Cups Becoming Popular Worldwide?

The rapid growth of takeaway beverages, specialty coffee culture, and premium café experiences has significantly increased global demand for double wall paper cups.

Consumers increasingly expect hot beverages to remain warm while still being comfortable to hold. Double wall construction addresses this need by providing improved insulation without requiring additional accessories such as paper sleeves, helping cafés streamline operations and reduce packaging complexity.

Brand presentation has also become an important purchasing consideration. The smooth outer wall provides a larger printable surface than ripple wall cups, allowing businesses to showcase logos, promotional graphics, seasonal campaigns, and brand storytelling more effectively.

In addition, coffee chains, hotels, restaurants, and foodservice operators are placing greater emphasis on customer experience. Premium beverage packaging is no longer viewed simply as a disposable container, but as an extension of the brand itself.

Advances in paper cup manufacturing technology have further improved printing quality, dimensional consistency, leak resistance, and production efficiency. As a result, modern double wall paper cups provide an excellent balance between functionality, aesthetics, and commercial value.

For importers, distributors, wholesalers, and beverage brands, double wall paper cups continue to represent one of the most attractive packaging categories for premium hot beverage service.


Industry Insights & Market Trends

The global coffee industry continues to expand, driven by changing consumer lifestyles, premium beverage consumption, and the rapid growth of takeaway and delivery services. As coffee consumption increases, beverage packaging is evolving from a simple disposable container into an important part of brand identity, customer experience, and sustainability strategy.

For manufacturers, distributors, and brand owners, understanding these market trends helps guide more informed packaging decisions and long-term sourcing strategies.
Double Wall Paper Cup Industry Insights & Market Trends


Global Market Overview

Coffee remains one of the world’s most widely consumed beverages, with billions of cups served every day through cafés, restaurants, offices, hotels, convenience stores, and takeaway channels.

At the same time, the demand for premium coffee experiences continues to rise. Consumers increasingly expect beverage packaging that not only performs well but also reflects the quality and values of the brands they purchase from.

This trend has contributed to the growing adoption of insulated paper cups, particularly double wall paper cups, which combine functionality, customer comfort, and premium branding opportunities.


Key Industry Trends

Premiumization of Coffee Packaging

Packaging has become an extension of the coffee brand rather than simply a disposable container.

Many coffee chains and specialty cafés now invest in custom printed cups, premium finishes, and consistent packaging designs to strengthen brand recognition and improve customer experience.


Growth of Takeaway and Delivery Consumption

The continued expansion of takeaway coffee and food delivery services has increased demand for packaging that performs reliably during transportation.

Insulation, secure lid compatibility, and leak resistance have become increasingly important purchasing criteria for commercial buyers.


Sustainability Is Becoming a Purchasing Requirement

Environmental considerations are influencing packaging decisions across many international markets.

Businesses are increasingly evaluating paper-based alternatives, renewable materials, recyclable packaging solutions, and lower-impact coating technologies alongside traditional purchasing criteria such as cost and functionality.

Rather than focusing on a single material, many buyers now seek packaging solutions that balance environmental objectives with commercial performance.


Brand Differentiation Through Packaging

For many beverage businesses, packaging serves as one of the most visible customer touchpoints.

High-quality printing, consistent colors, and premium cup construction help create a stronger brand image and improve customer perception long after the beverage has been served.


Regional Market Focus

Different regions prioritize different aspects of disposable beverage packaging.

Region

Typical Market Focus

North America

Product performance, branding, operational efficiency

Europe

Sustainability, regulatory compliance, recyclable and compostable solutions

Australia & New Zealand

Environmental performance, premium takeaway experience

Middle East

Premium presentation, heat resistance, hospitality applications

Asia

Cost efficiency, production stability, rapid delivery

Understanding these regional priorities enables buyers to select packaging solutions that better align with local customer expectations and market conditions.

What This Means for Buyers

Today’s purchasing decisions are no longer based solely on product price.

Professional buyers increasingly evaluate suppliers based on their ability to deliver:

  • Consistent product quality
  • Reliable manufacturing capacity
  • Flexible customization
  • Food-contact compliance support
  • Stable long-term supply
  • Sustainable packaging options
  • Technical expertise

As the beverage packaging industry continues to evolve, successful sourcing depends on selecting solutions that support not only current operational needs but also future market developments.

Businesses that combine high-quality products with strategic packaging planning are better positioned to strengthen customer satisfaction, improve operational efficiency, and build long-term competitive advantage.


Material Comparison Guide

Selecting the right material is one of the most important decisions when sourcing disposable coffee cups. The ideal solution depends not only on insulation performance, but also on cost, sustainability objectives, local regulations, consumer expectations, and end-of-life waste management.

The following comparison helps buyers evaluate the most common hot beverage cup materials from a commercial procurement perspective.

Evaluation Criteria

Double Wall Paper Cup (PE)

Double Wall Paper Cup (PLA)

Water-Based Barrier Paper Cup

Bagasse Coffee Cup

Plastic Cup (PP/PS)

Primary Material

Virgin Paperboard + PE

Virgin Paperboard + PLA

Virgin Paperboard + Water-Based Barrier

Sugarcane Fiber

Petroleum-Based Plastic

Insulation Performance

Excellent

Excellent

Excellent

Good

Fair

Printing Quality

Excellent

Excellent

Excellent

Moderate

Good

Premium Brand Presentation

Excellent

Excellent

Excellent

Natural Appearance

Standard

Hot Beverage Performance

Excellent

Excellent

Excellent

Excellent

Limited

Cold Beverage Performance

Good

Good

Good

Good

Excellent

Typical Unit Cost

$$

$$$

$$$

$$$

$

Production Availability

Excellent

Good

Developing

Good

Excellent

OEM Customization

Excellent

Excellent

Good

Good

Excellent

Food Contact Compliance

Available

Available

Available

Available

Available

Industrial Compostability

No

Yes*

Depends on Local Standards

Yes*

No

Recyclability**

Limited

Limited

Improved in Some Markets

Limited

Depends on Local Systems

Consumer Sustainability Perception

Good

Excellent

Excellent

Excellent

Low

Suitable Markets

Global

Europe, Australia

Europe, Selected Markets

Global Sustainable Packaging

Cost-Sensitive Markets

Recommended Applications

Coffee Chains, Cafés, Hospitality

Premium Sustainable Brands

Plastic Reduction Programs

Eco-Friendly Foodservice

Cold Beverage Programs

Compostability depends on product certification and the availability of industrial composting facilities.

Actual recyclability depends on local collection, sorting, and recycling infrastructure.
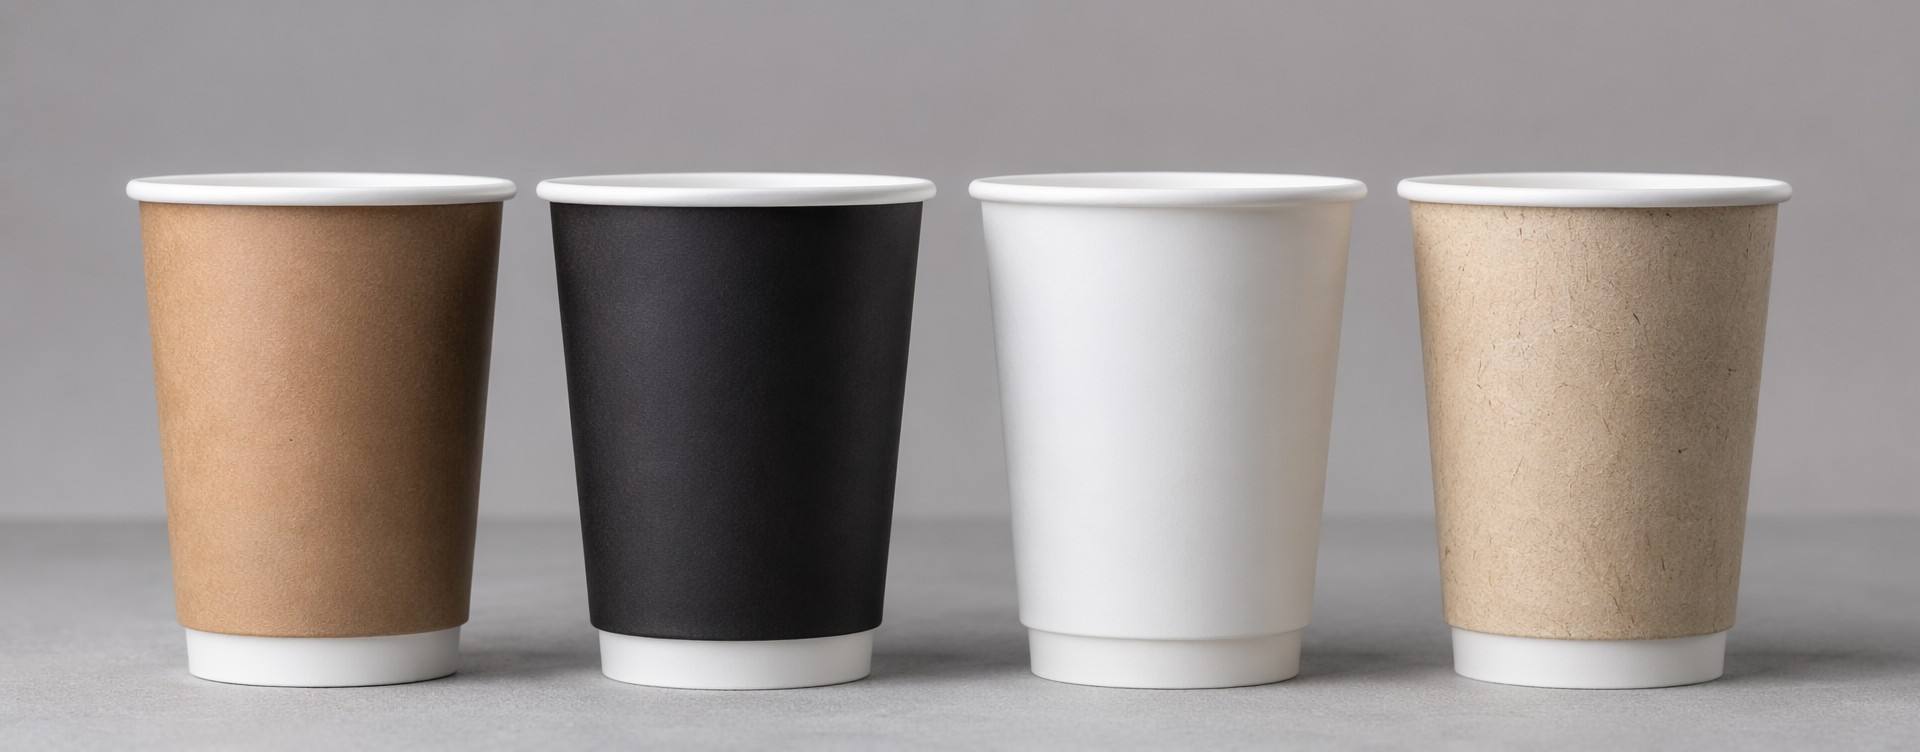
Double Wall Paper Cup Material Comparison Guide


Which Material Is Right for Your Business?

Every material offers different advantages depending on your business model and target market.

Choose PE-Coated Double Wall Paper Cups If You:

  • Prioritize reliable performance and competitive cost.
  • Supply coffee shops, restaurants, or foodservice distributors.
  • Export to markets where PE-coated paper cups remain widely accepted.
  • Require stable large-scale production capacity.


Choose PLA-Coated Double Wall Paper Cups If You:

  • Target markets with industrial composting infrastructure.
  • Need packaging that supports certified compostable programs.
  • Serve environmentally conscious brands seeking bio-based coating solutions.


Choose Water-Based Barrier Paper Cups If You:

  • Focus on markets promoting plastic reduction and fiber recycling.
  • Want to explore next-generation recyclable paper cup technologies.
  • Require innovative packaging solutions aligned with evolving regulations.


Choose Bagasse Coffee Cups If You:

  • Want to emphasize renewable plant-fiber packaging.
  • Prefer a natural molded fiber appearance.
  • Position your brand around sustainability and agricultural resource utilization.
  • Do not require high-definition full-surface printing.


Choose Plastic Cups If You:

  • Primarily serve cold beverages.
  • Prioritize the lowest initial packaging cost.
  • Operate in applications where thermal insulation is not required.


Procurement Recommendations by Market

Different regions have different packaging priorities. Selecting the appropriate material according to your target market can reduce compliance risks and improve customer acceptance.

Target Market

Recommended Material

Primary Purchasing Considerations

North America

PE / PLA Double Wall Paper Cup

Performance, Branding, Food Contact Compliance

Europe

PLA / Water-Based Barrier / Fiber Solutions

Sustainability, Compostability, Plastic Reduction

Australia & New Zealand

PLA / Water-Based Barrier

Compostability, Environmental Compliance

Middle East

PE Double Wall Paper Cup

Heat Resistance, Premium Presentation

Asia

PE Double Wall Paper Cup

Cost Efficiency, Stable Supply

Hospitality & Coffee Chains

Double Wall Paper Cup

Customer Experience, Brand Visibility

Eco-Focused Brands

Bagasse Coffee Cup / PLA Cup

Renewable Materials, Sustainability Messaging

Rather than selecting a material based on a single characteristic, buyers are encouraged to evaluate performance, regulatory requirements, branding objectives, operational efficiency, and total procurement cost together. This approach helps identify the most suitable packaging solution for long-term business success.


DAILYECO’s Complete Double Wall Paper Cup Categories Will Cover All Your Sales and On-Site Application Needs

DAILYECO offers a complete range of double wall paper cups designed for coffee shops, cafés, restaurant chains, foodservice distributors, hospitality groups, convenience stores, and private-label beverage packaging brands.

Our product portfolio covers the most used capacities for espresso, coffee, tea, and specialty hot beverages. Each size is engineered to provide excellent insulation, comfortable handling, and compatibility with a wide range of paper and plastic lids.

Size

Top Diameter (mm)

Bottom Diameter (mm)

Height (mm)

Standard Packing

Carton Size (cm)

4oz double wall paper cup

62

45

60

25 pcs × 20 sleeves

40 × 26 × 32

8oz double wall paper cup

80

56

90

25 pcs × 20 sleeves

48.5 × 33 × 41

10oz double wall paper cup

90

60

95

25 pcs × 20 sleeves

45.5 × 36.5 × 39

12oz double wall paper cup

90

60

110

25 pcs × 20 sleeves

46 × 37 × 47.5

16oz double wall paper cup

90

60

136

25 pcs × 20 sleeves

56 × 46 × 37

20oz double wall paper cup

90

60

150

25 pcs × 20 sleeves

46 × 37 × 67

22oz double wall paper cup

90

60

170

25 pcs × 20 sleeves

46 × 38 × 75


All specifications can be customized according to your market requirements, branding strategy, and beverage menu.


Customization Options

DAILYECO provides comprehensive OEM and private-label solutions for beverage brands, distributors, and packaging companies worldwide.

Customization services include:

  • Custom Logo Printing
  • CMYK Full Surface Printing
  • Pantone Color Matching
  • Matte or Gloss Finish
  • Custom Cup Size Development
  • Custom Packaging Design
  • Private Label Solutions
  • Retail Packaging
  • Amazon Ready Packaging
  • Barcode Printing
  • QR Code Printing
  • Seasonal Promotional Designs

Our engineering and printing teams work closely with customers to ensure each project accurately reflects brand identity while maintaining consistent production quality.
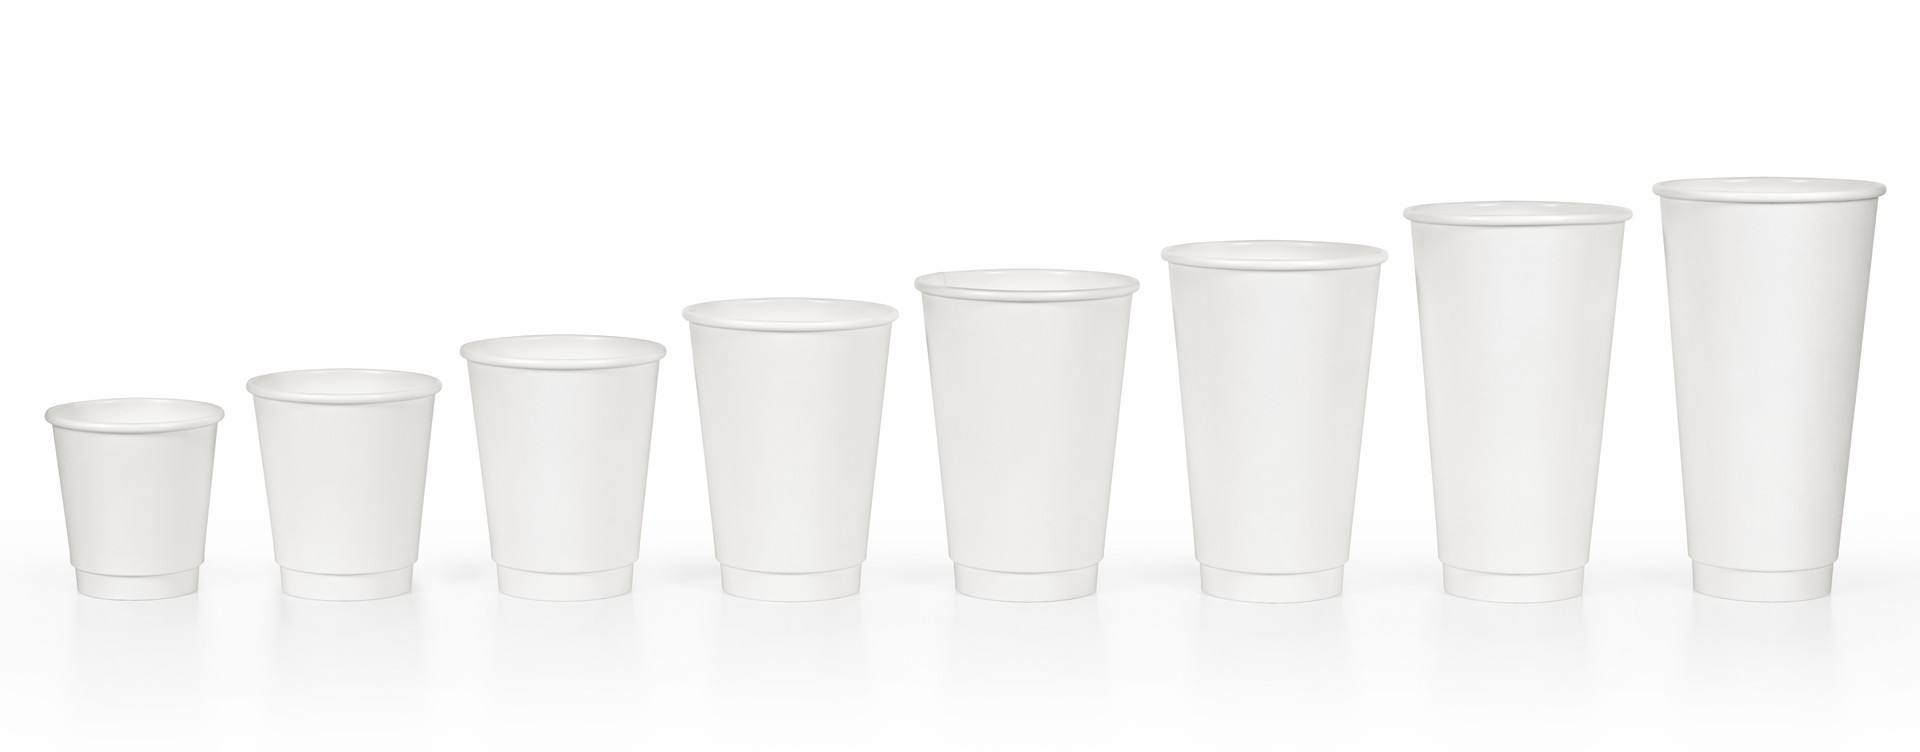
Double Wall Paper Cup Size Guide 

Coffee Cup Size Guide

Selecting the appropriate cup size helps improve beverage presentation, operational efficiency, and customer satisfaction.

Size

Typical Beverage

4oz

Espresso

6oz

Flat White

8oz

Cappuccino

10oz

Americano

12oz

Latte

16oz

Large Coffee

20oz

Extra Large Coffee & Specialty Drinks

22oz

Boba Tea

Different markets may use different naming conventions and serving sizes. DAILYECO can recommend the most suitable specifications according to your target market and beverage program.
Get Latest Catalog

What Is the Application of Double Wall Paper Cups? 

Double wall paper cups are widely used across the global foodservice and beverage industry. Their excellent thermal insulation, premium appearance, and branding capabilities make them a preferred packaging solution for businesses serving hot beverages.

The following guide explains not only where double wall paper cups are used, but also why different industries choose them and what purchasing considerations are typically involved.

Branded Double Wall Paper Cups for Coffee Shops

Takeaway Coffee Service

Takeaway coffee remains the largest application for double wall paper cups worldwide.

Customers expect beverages to stay warm while remaining comfortable to hold during transport. The double wall construction reduces the need for additional sleeves and provides an excellent surface for custom branding.

Typical Requirements

  • Excellent heat insulation
  • Comfortable grip
  • Secure lid fit
  • Premium brand presentation
  • Multiple cup sizes

Recommended Sizes

8oz · 12oz · 16oz

Office Beverage Programs

Corporate offices, business parks, and co-working spaces increasingly provide self-service coffee stations for employees and visitors.

Packaging in these environments should be practical, clean, and easy to manage while maintaining a professional appearance.

Typical Requirements

  • Cost-effective standard specifications
  • Comfortable handling
  • Easy inventory management
  • Reliable daily supply

Recommended Sizes

8oz · 12oz

Double Wall Paper Cups Used in Office Coffee Programs
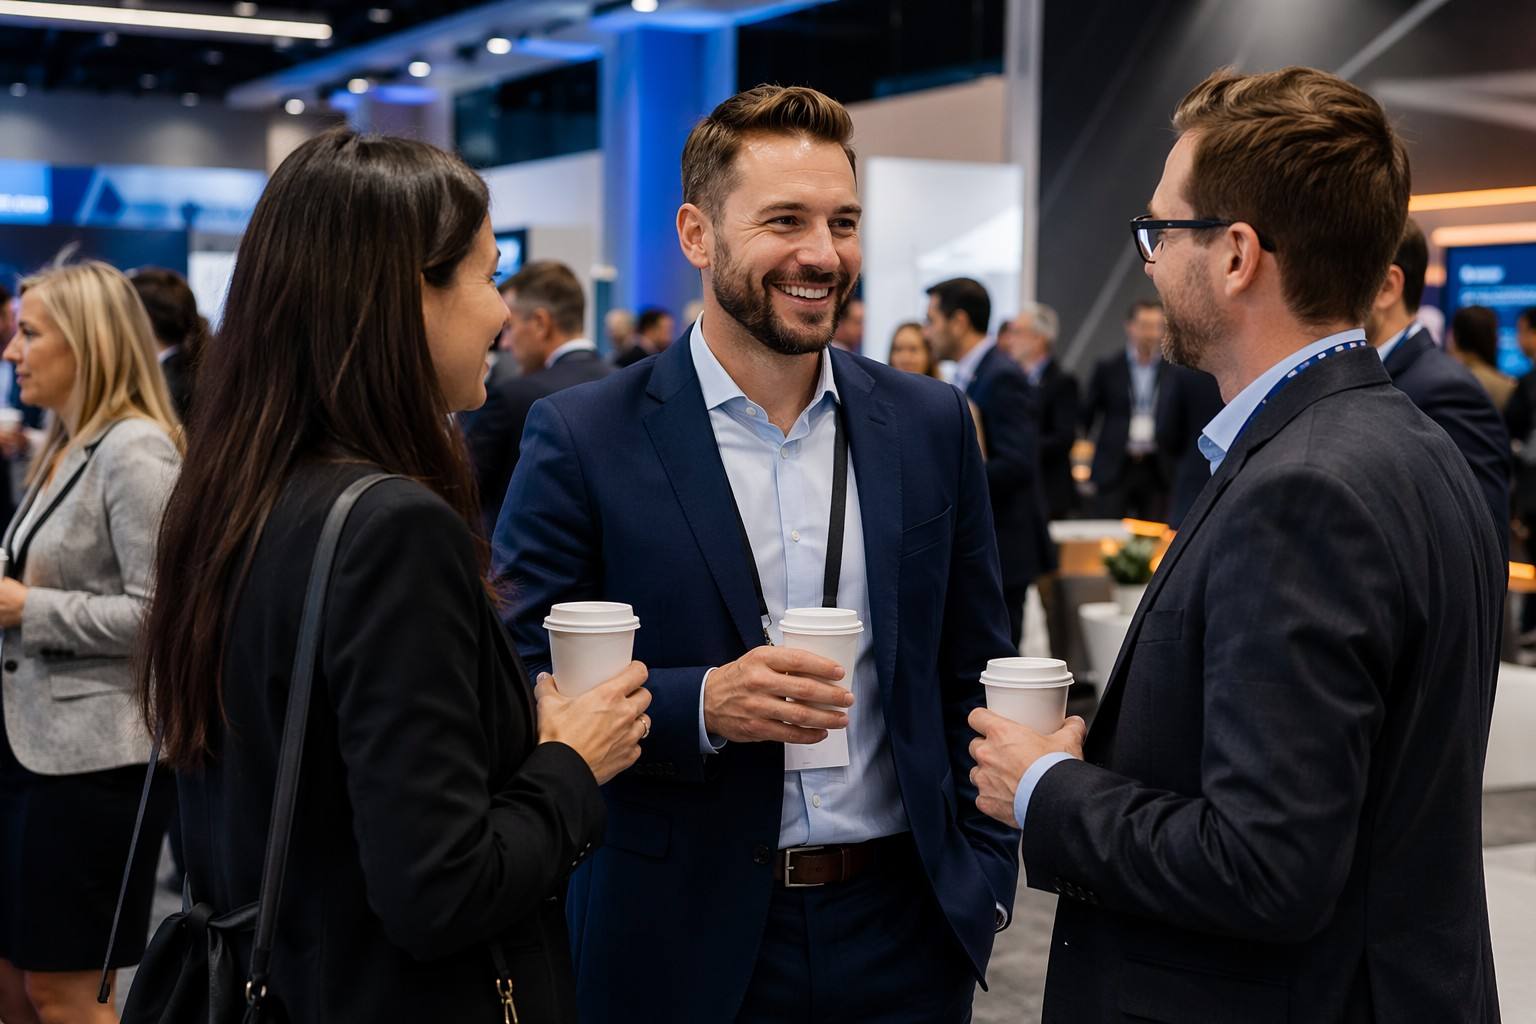
Double Wall Paper Cups for Conferences and Exhibitions

Conference & Exhibition Beverage Service

Business conferences, exhibitions, seminars, and trade shows often serve thousands of hot beverages within a short period.

Double wall paper cups improve attendee comfort while providing valuable branding opportunities for sponsors and organizers.

Typical Requirements

  • Fast delivery
  • Consistent printing quality
  • Event branding
  • Reliable leak resistance

Recommended Sizes

8oz · 12oz

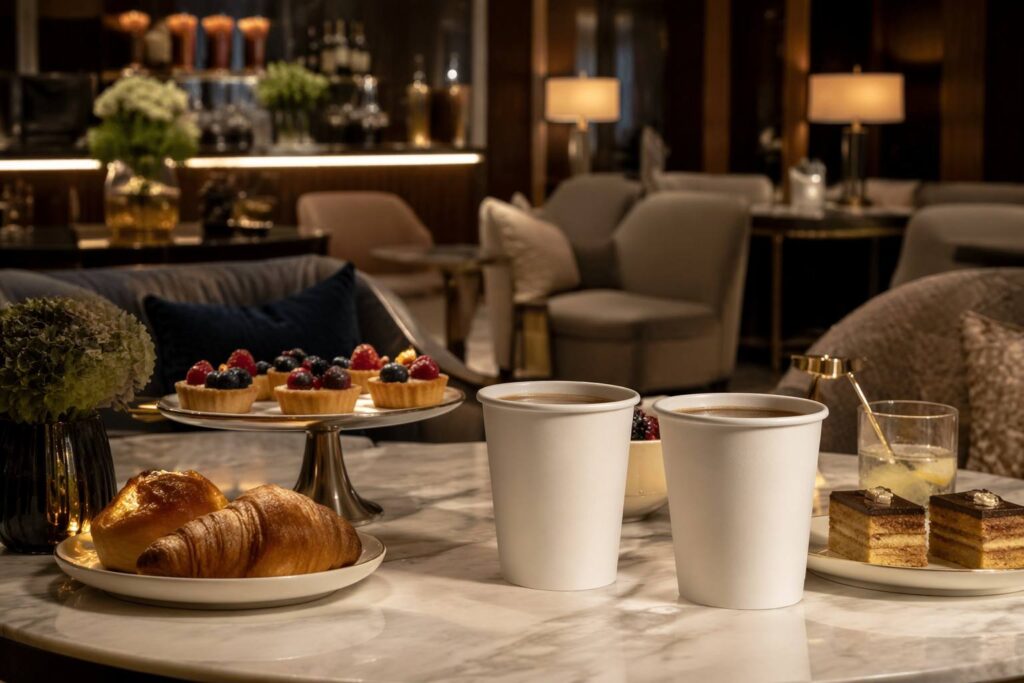
Hotel & Guest Hospitality

Hotels commonly use insulated paper cups for breakfast buffets, executive lounges, room service, meeting facilities, and guest welcome areas.

Premium beverage packaging contributes to the overall guest experience.

Typical Requirements

  • Premium appearance
  • Food-contact safety
  • High-quality printing
  • Stable year-round supply

Recommended Sizes

8oz · 12oz

Premium Double Wall Paper Cups for Hotel Hospitality
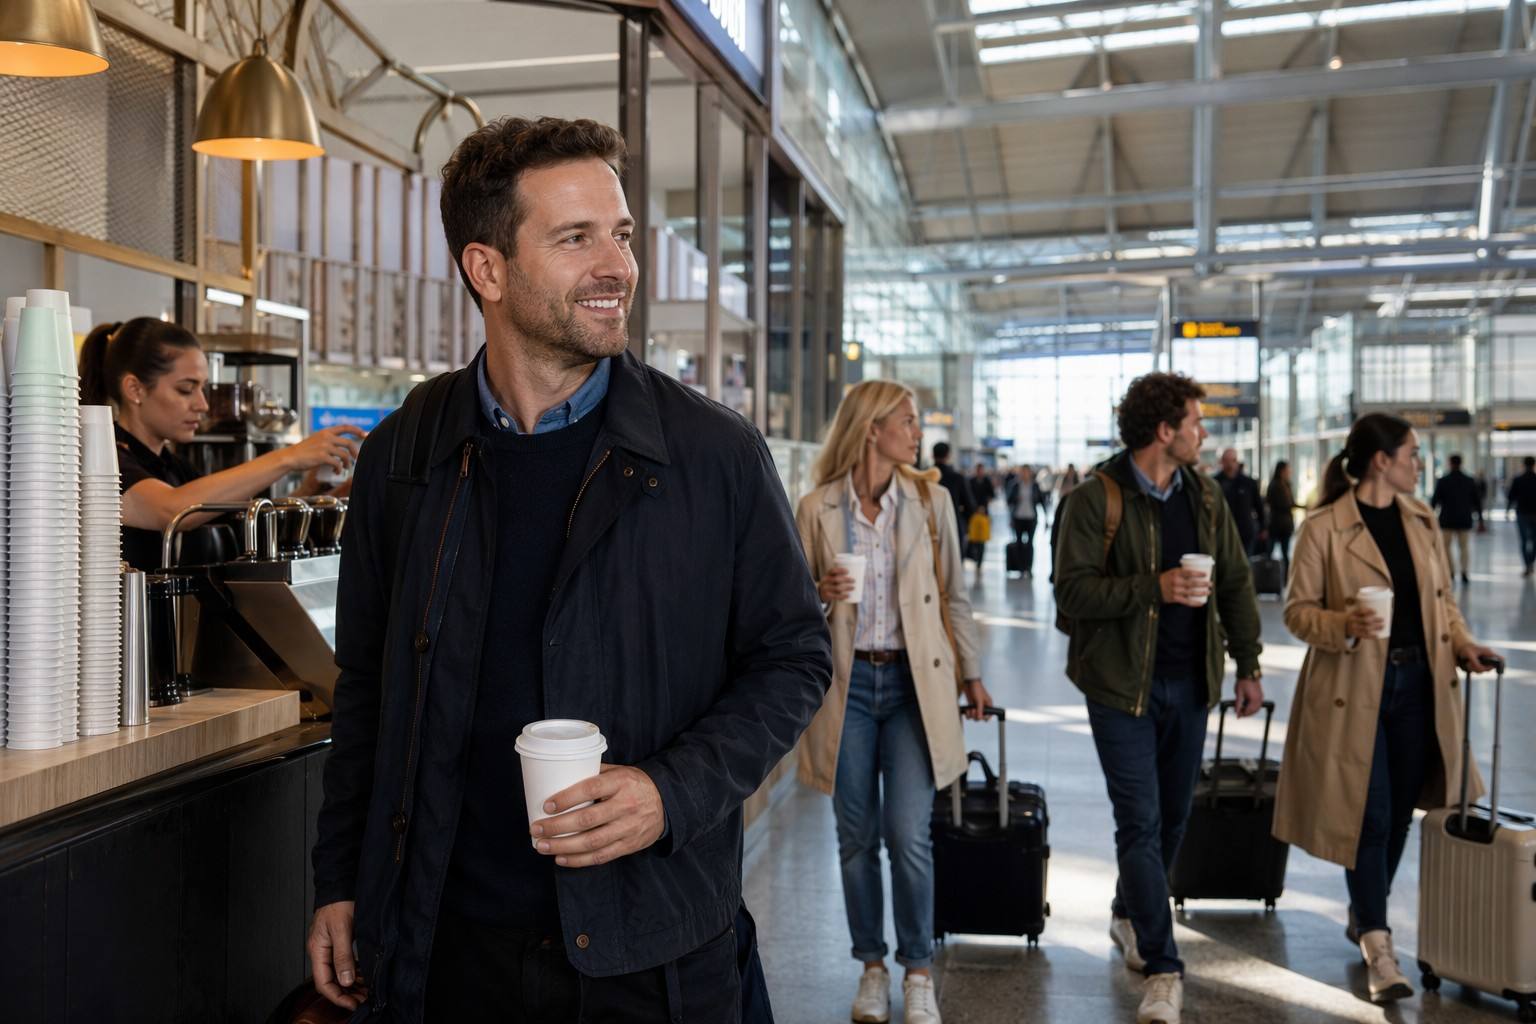
Double Wall Paper Cups for Airport and Railway Beverage Service

Transportation & Travel Beverage Service

Airports, railway stations, highway service areas, and travel operators require beverage packaging that performs well during customer movement.

Reliable insulation and secure lid compatibility help improve the overall takeaway experience.

Typical Requirements

  • Leak resistance
  • Comfortable handling
  • Lightweight packaging
  • High-volume availability

Recommended Sizes

8oz · 12oz · 16oz

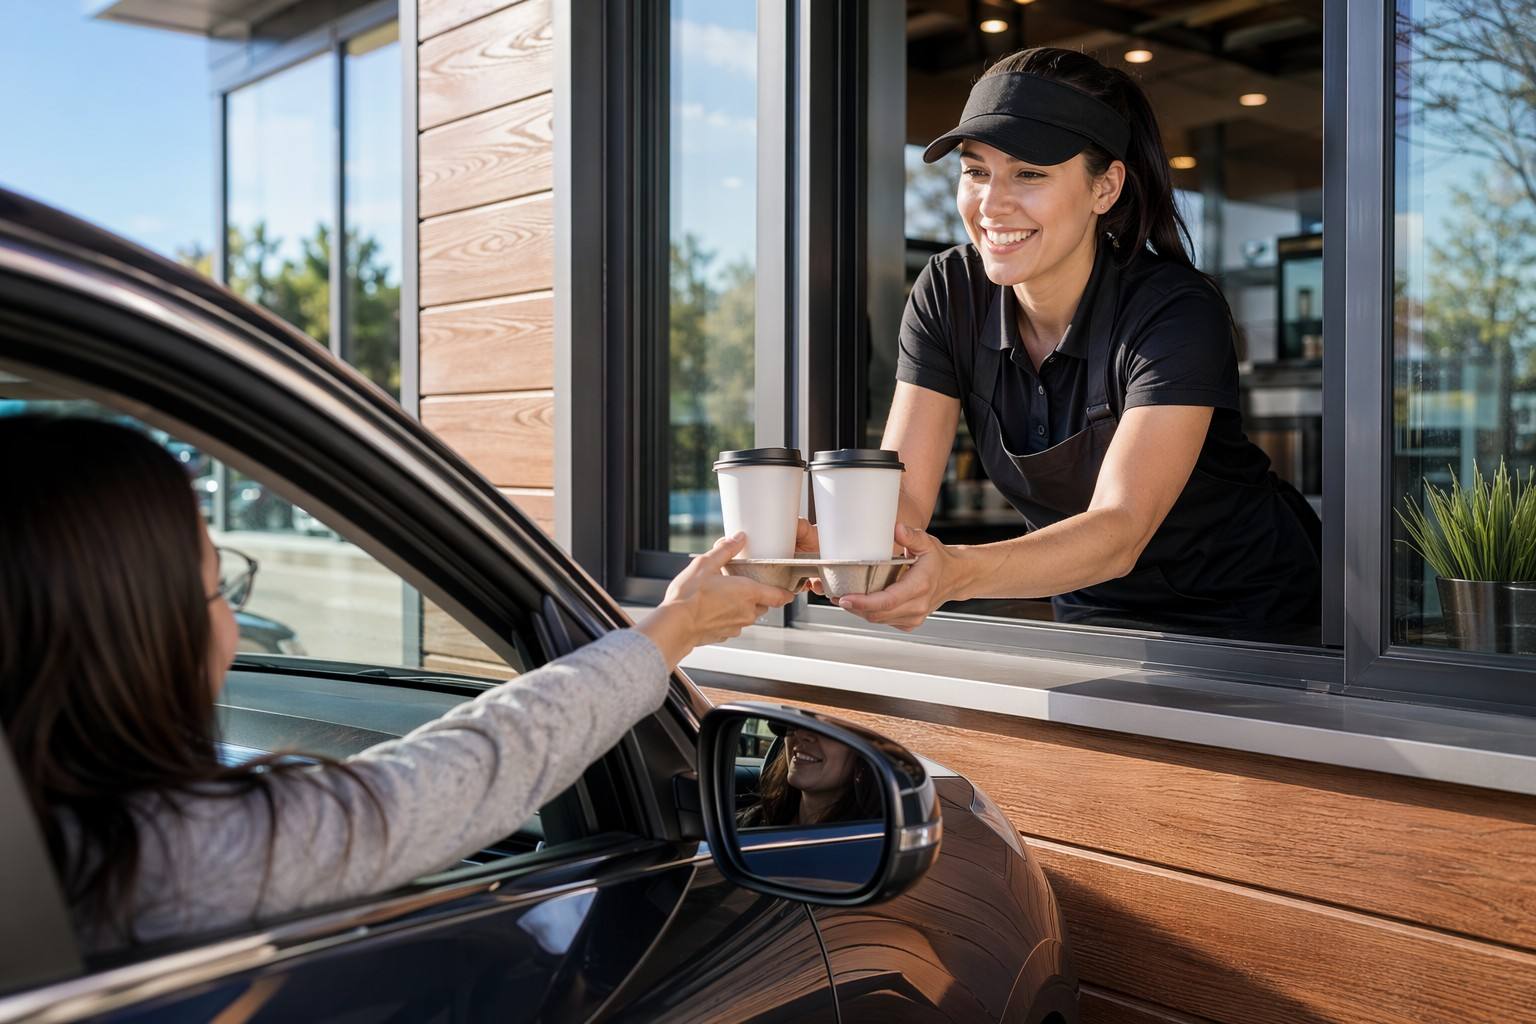
Drive-Through & Quick Service Restaurants

Quick-service restaurants and drive-through coffee programs emphasize speed, consistency, and operational efficiency.

Packaging must support fast preparation while maintaining product quality during transportation.

Typical Requirements

  • Standardized specifications
  • Fast service
  • Reliable lid compatibility
  • Consistent quality

Recommended Sizes

12oz · 16oz

Double Wall Paper Cups for Drive-Through Coffee Service
Double Wall Paper Cups for Coffee Delivery Services

Food Delivery Platforms

With the continued growth of online food delivery, beverage packaging must maintain temperature and minimize leakage throughout transportation.

A properly matched cup-and-lid system improves customer satisfaction and reduces complaints.

Typical Requirements

  • Secure sealing
  • Transportation performance
  • Brand visibility
  • Delivery durability

Recommended Sizes

12oz · 16oz

Outdoor Events & Seasonal Promotions

Music festivals, sporting events, seasonal markets, promotional campaigns, and temporary coffee kiosks require beverage packaging that is lightweight, attractive, and easy to distribute.

Custom printed double wall paper cups also provide excellent promotional visibility.

Typical Requirements

  • Custom printing
  • Flexible order quantities
  • Easy transportation
  • Strong visual branding

Recommended Sizes

8oz · 12oz · 16oz

Custom Double Wall Paper Cups for Outdoor Events and Promotions

Double Wall Paper Cups vs Other Disposable Coffee Cups

Selecting the right disposable coffee cup requires balancing thermal insulation, customer experience, branding opportunities, sustainability objectives, and overall packaging cost. Different cup constructions are designed for different beverage applications, and understanding their differences helps buyers choose the most suitable solution.


Double Wall Paper Cups vs Single Wall Paper Cups

Factor

Double Wall Paper Cup

Single Wall Paper Cup

Wall Construction

Double Layer

Single Layer

Heat Insulation

Excellent

Standard

Sleeve Requirement

Usually Not Required

Often Required

Customer Comfort

Excellent

Moderate

Printing Area

Excellent

Excellent

Material Consumption

Higher

Lower

Packaging Cost

Medium

Lower

Typical Applications

Premium Coffee, Takeaway

Offices, Schools, General Beverage Service

Single wall paper cups remain an economical option for many beverage businesses. However, for hot drinks served directly to customers, double wall paper cups provide significantly better insulation and a more premium drinking experience without requiring an additional sleeve.


Double Wall Paper Cups vs Ripple Wall Paper Cups

Factor

Double Wall Paper Cup

Ripple Wall Paper Cup

Insulation Performance

Excellent

Excellent

Customer Grip

Smooth Surface

Textured Surface

Printing Quality

Excellent

Moderate

Premium Branding

Excellent

Good

Sleeve Requirement

No

No

Manufacturing Complexity

Medium

Higher

Typical Applications

Coffee Chains, Premium Cafés

Coffee Shops, Convenience Stores

Both products provide excellent thermal insulation. Double wall paper cups offer a larger and smoother printable surface, making them particularly suitable for businesses that prioritize visual branding and premium packaging presentation. Ripple wall cups provide additional grip through their corrugated outer layer and are often selected for high-volume takeaway operations.


Double Wall Paper Cups vs PE-Coated Paper Cups

Factor

Double Wall Paper Cup

Standard PE-Coated Paper Cup

Insulation

Excellent

Standard

Sleeve Requirement

Usually No

Often Yes

Customer Experience

Premium

Standard

Printing Surface

Large

Standard

Hot Beverage Performance

Excellent

Excellent

Typical Users

Coffee Brands, Hospitality

General Foodservice

PE-coated paper cups remain one of the most common disposable beverage packaging solutions. Double wall paper cups use similar food-grade materials while adding a second paper layer to improve insulation and customer comfort.


Double Wall Paper Cups vs Plastic Cups

Factor

Double Wall Paper Cup

Plastic Cup

Hot Beverage Suitability

Excellent

Limited

Insulation

Excellent

Poor

Branding Appearance

Premium

Standard

Renewable Paper Content

High

None

Consumer Perception

Premium

Declining in Many Markets

Typical Beverage

Coffee, Tea

Cold Drinks

Plastic cups continue to perform well in cold beverage applications. However, for coffee, tea, and other hot beverages, double wall paper cups provide a safer, more comfortable, and more brand-focused packaging solution.


Double Wall Paper Cups vs Bagasse Coffee Cups

Factor

Double Wall Paper Cup

Bagasse Coffee Cup

Primary Material

Paperboard

Sugarcane Fiber

Thermal Insulation

Excellent

Good

Printing Quality

Excellent

Limited

Premium Brand Presentation

Excellent

Good

Surface Finish

Smooth

Natural Fiber Texture

Custom Graphic Printing

Excellent

Limited

Typical Positioning

Premium Coffee Packaging

Sustainable Fiber Packaging

Both products serve the hot beverage market but emphasize different priorities. Double wall paper cups are often selected when premium branding, vibrant printing, and customer comfort are the primary considerations. Bagasse coffee cups are typically preferred by brands emphasizing natural materials and fiber-based sustainability.

Who Usually Buys Double Wall Paper Cups?

Double wall paper cups are primarily purchased by businesses rather than end consumers. Different buyer groups have different purchasing priorities, from cost control and supply stability to brand consistency and product customization.

Understanding who your customers are—and what they value most—helps suppliers provide more targeted solutions and build stronger long-term partnerships.

Importer Reviewing Double Wall Paper Cup Samples

Importers

Importers typically purchase double wall paper cups in full-container quantities and distribute them within their domestic markets. Their focus is on stable product quality, competitive pricing, efficient logistics, and reliable export support.

Packaging Distributors

Packaging distributors maintain inventory covering multiple cup sizes and accessories to supply cafés, restaurants, offices, and foodservice businesses. Product availability and fast replenishment are key competitive advantages.

Packaging Distributor Stocking Double Wall Paper Cups
Coffee Chain Procurement Team Reviewing Custom Paper Cups

Coffee Chain Procurement Teams

Regional and international coffee chains usually purchase through centralized procurement departments responsible for maintaining consistent packaging across all store locations.

For these buyers, supply stability and brand consistency are often more important than achieving the lowest unit price.

Brand Owners

Brand owners view packaging as an extension of their customer experience. Double wall paper cups are selected not only for insulation performance but also for premium printing and brand visibility.

Brand Owner Reviewing Custom Double Wall Paper Cup Designs
Private Label Double Wall Paper Cup Manufacturing

Private Label Packaging Companies

Private-label packaging companies cooperate with manufacturers to develop customized paper cups under their own brands. Confidential production, stable quality, and flexible customization are essential.

Foodservice Supply Companies

Foodservice suppliers provide complete packaging solutions to restaurants, hotels, schools, hospitals, catering companies, and institutional customers. They typically require broad product portfolios rather than a single paper cup specification.

Food service Supplier Managing Sustainable Packaging Inventory
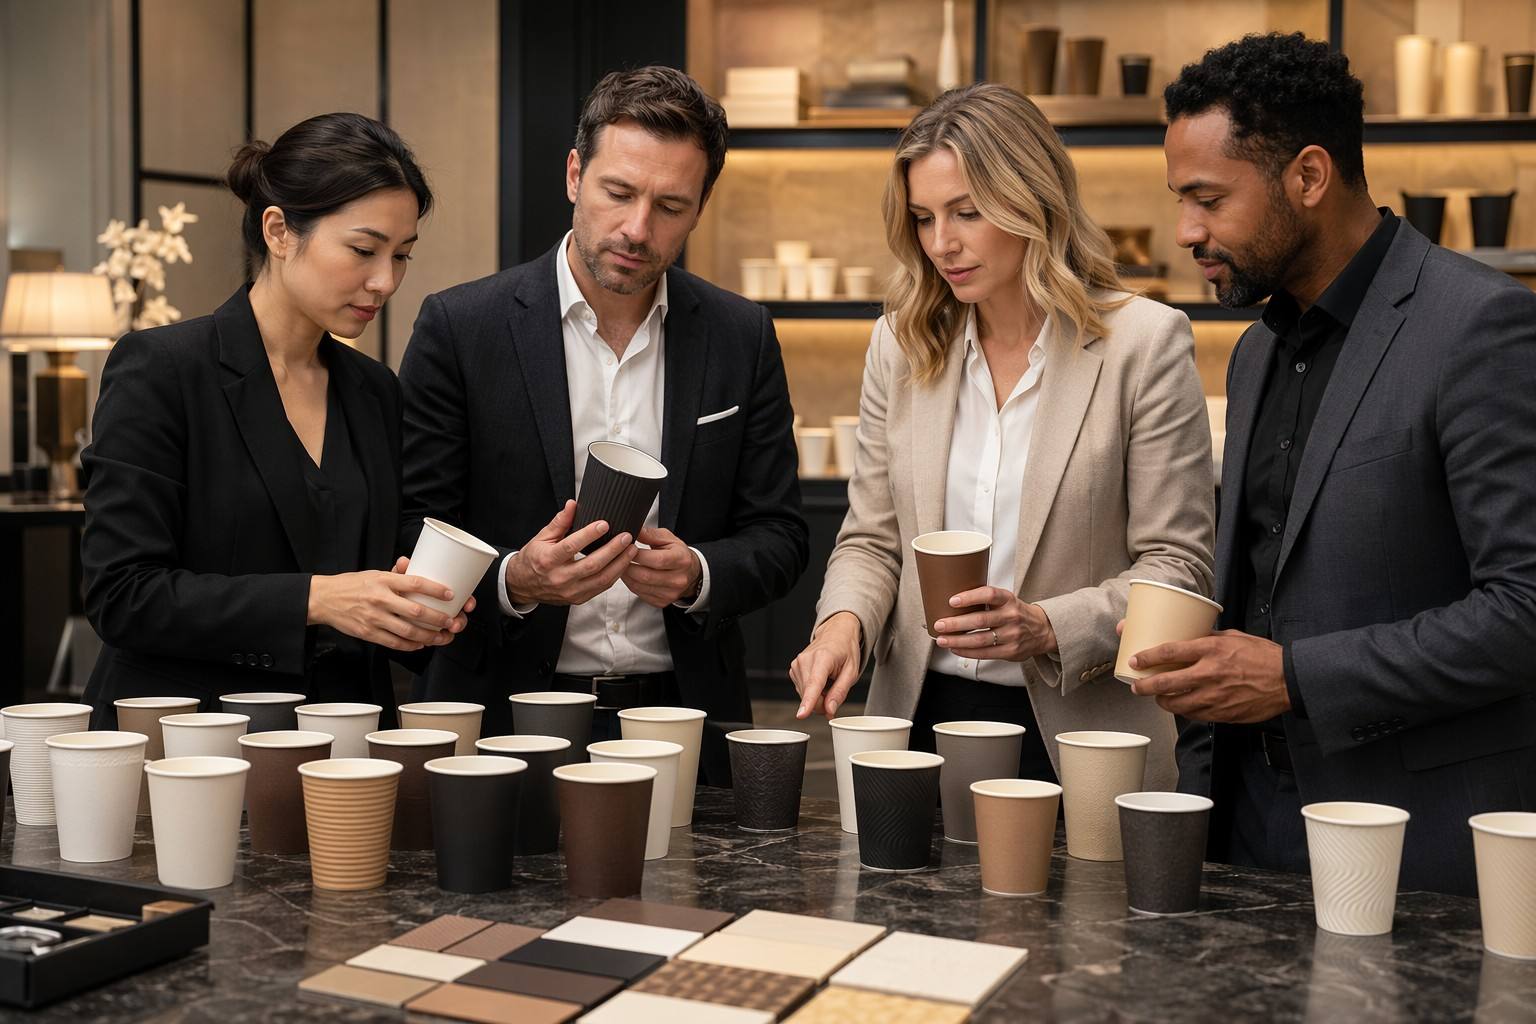
Hospitality Procurement Team Evaluating Double Wall Paper Cups

Hospitality Procurement Companies

Hospitality procurement companies purchase beverage packaging for hotel groups, resorts, conference centers, and catering operations. Their focus is on product quality, guest experience, and dependable long-term supply.

E-commerce Packaging Brands

Many e-commerce packaging brands build their product portfolios around customized, retail-ready packaging sold through online marketplaces. They often require flexible development support, attractive packaging, and efficient supply for new product launches.

E-commerce Packaging Brand Developing Custom Double Wall Paper Cups

Is Double Wall Paper Cup Right for Your Application? 

The following guide helps buyers determine whether double wall paper cups are suitable for different commercial beverage applications.

Application

Recommended

Espresso

Americano

Cappuccino

Latte

Flat White

Tea Service

Hot Chocolate

Office Coffee Programs

Takeaway Coffee

Food Delivery

Hotel Beverage Service

Conference Catering

Restaurant Beverage Service

Convenience Store Coffee

Long-Term Liquid Storage

Industrial Liquid Applications

Double wall paper cups are specifically designed for short-term hot beverage consumption in commercial foodservice environments. They provide excellent insulation, comfortable handling, and strong branding opportunities for takeaway and dine-in beverage service.

For applications requiring long-term liquid storage, industrial chemical resistance, or extended transportation of liquids, alternative packaging solutions should be considered.


Key Buyer Questions Before Purchasing Double Wall Paper Cups

Choosing the right double wall paper cup involves more than selecting a size. Buyers should evaluate insulation performance, material options, printing requirements, lid compatibility, and supplier capabilities before placing an order.

Are double wall paper cups suitable for hot beverages?

Yes. Double wall paper cups are specifically designed for hot beverages such as coffee, tea, cappuccino, latte, hot chocolate, and other specialty drinks. The additional outer paper layer reduces heat transfer while helping beverages retain their serving temperature.


Do double wall paper cups require paper sleeves?

In most applications, no.

The double wall construction creates an insulating air gap between the inner and outer walls, allowing customers to comfortably hold hot beverages without requiring an additional paper sleeve.

However, for extremely hot beverages or oversized cups, some coffee brands may still choose to use sleeves as part of their brand presentation.


Which coating option should I choose?

The most suitable coating depends on your target market and local packaging regulations.

Typical options include:

  • PE coating for excellent liquid resistance and cost-effective production.
  • PLA coating for markets requiring industrial compostable packaging.
  • Water-based barrier coatings for customers pursuing recyclable fiber-based packaging solutions.

DAILYECO can recommend the most appropriate material based on your export destination and sustainability objectives.


Can double wall paper cups be customized?

Yes.

DAILYECO supports comprehensive customization services, including:

  • Custom logo printing
  • Full-color graphics
  • Pantone color matching
  • Matte and glossy finishes
  • QR codes
  • Private label branding
  • Retail-ready packaging
  • Custom carton printing


What cup sizes are commonly available?

The most popular capacities include:

  • 4 oz
  • 6 oz
  • 8 oz
  • 10 oz
  • 12 oz
  • 16 oz
  • 20 oz

Additional sizes may be developed according to project requirements.


Which lids are compatible?

Depending on the application, double wall paper cups can be paired with:

  • Paper lids
  • PP sip lids
  • PS lids
  • Dome lids
  • Flat lids

Selecting the correct lid improves leak resistance, transportation safety, and customer experience.


Are double wall paper cups recyclable?

Recyclability depends on the coating material used and the recycling infrastructure available in the destination market.

Many regions continue expanding recycling capabilities for paper beverage packaging. Buyers should evaluate local waste management systems when selecting coating options.


Are food-contact compliant materials available?

Yes.

DAILYECO manufactures products using food-grade paperboard and can support applicable food-contact compliance documentation according to customer requirements and destination markets.


Can these cups be used for takeaway coffee?

Absolutely.

Double wall paper cups are one of the most widely used packaging solutions for takeaway coffee because they combine thermal insulation, customer comfort, premium branding, and reliable transportation performance.


Is OEM manufacturing available?

Yes.

DAILYECO provides OEM and ODM manufacturing services for global distributors, wholesalers, coffee chains, hospitality groups, and private-label beverage packaging brands.
Frequently Asked Questions About Double Wall Paper Cups


When Double Wall Paper Cups May Not Be the Best Choice

Although double wall paper cups are widely used for premium hot beverage service, they may not be the ideal solution for every application.

Understanding these limitations helps buyers choose the most appropriate packaging solution for their business.


Extremely Cost-Sensitive Projects

For projects where minimizing unit cost is the highest priority, single wall paper cups may offer a more economical alternative, although additional sleeves may be required for hot beverages.


Long-Term Liquid Storage

Double wall paper cups are designed for immediate beverage consumption rather than prolonged liquid storage.

For products requiring extended storage or shelf-life after filling, specialized packaging solutions should be evaluated.


Cold Beverage Programs

Although double wall paper cups can be used for cold beverages, single wall paper cups or transparent PLA and PET cups are often more cost-effective for iced drinks where thermal insulation is unnecessary.


Industrial Applications

Double wall paper cups are intended for commercial foodservice and beverage packaging.

They are not designed for industrial liquid handling, laboratory applications, or chemical storage.


Applications Requiring Maximum Sustainability Positioning

For brands whose primary objective is emphasizing natural plant-fiber packaging, molded fiber products such as bagasse coffee cups may better align with their sustainability messaging.

Understanding the intended application before purchasing helps buyers select packaging that balances performance, branding, regulatory compliance, and overall cost.
What Is the Processing to Manufacture Double Wall Paper Cups? 

Producing high-quality double wall paper cups requires precision manufacturing to ensure reliable insulation, accurate dimensions, leak resistance, and premium printing quality.

The production process combines advanced paper converting technology with strict quality control procedures.

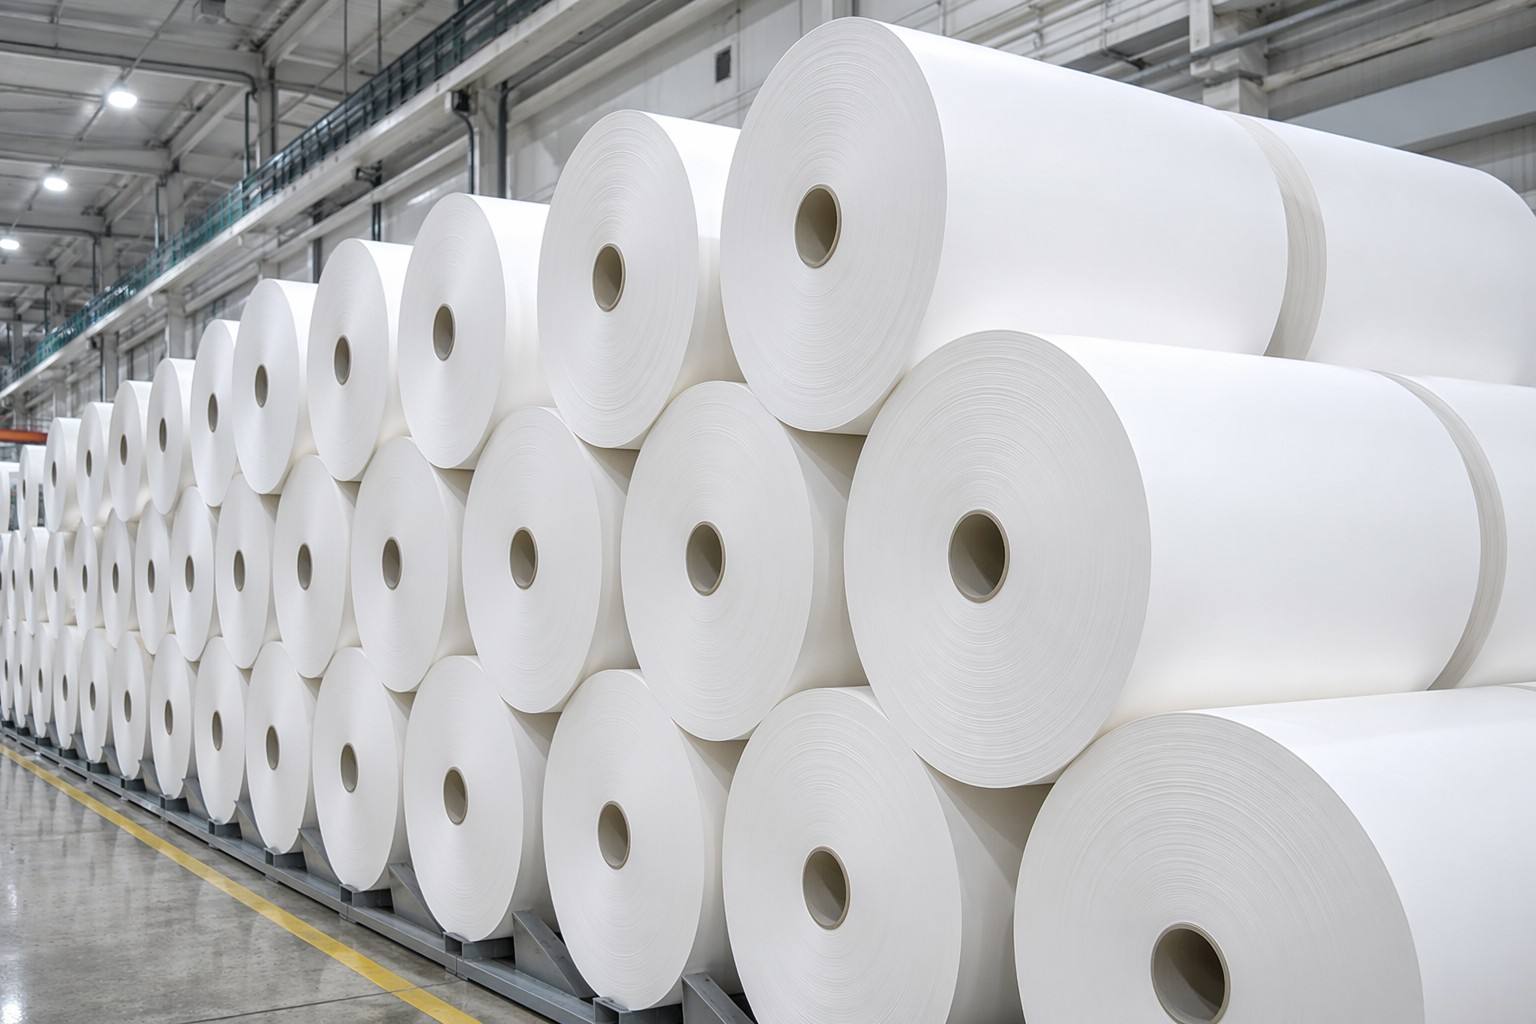
Food-Grade Paperboard for Double Wall Paper Cups

Step 1 – Paperboard Selection

Food-grade paperboard is carefully selected according to grammage, stiffness, printability, and food-contact requirements.

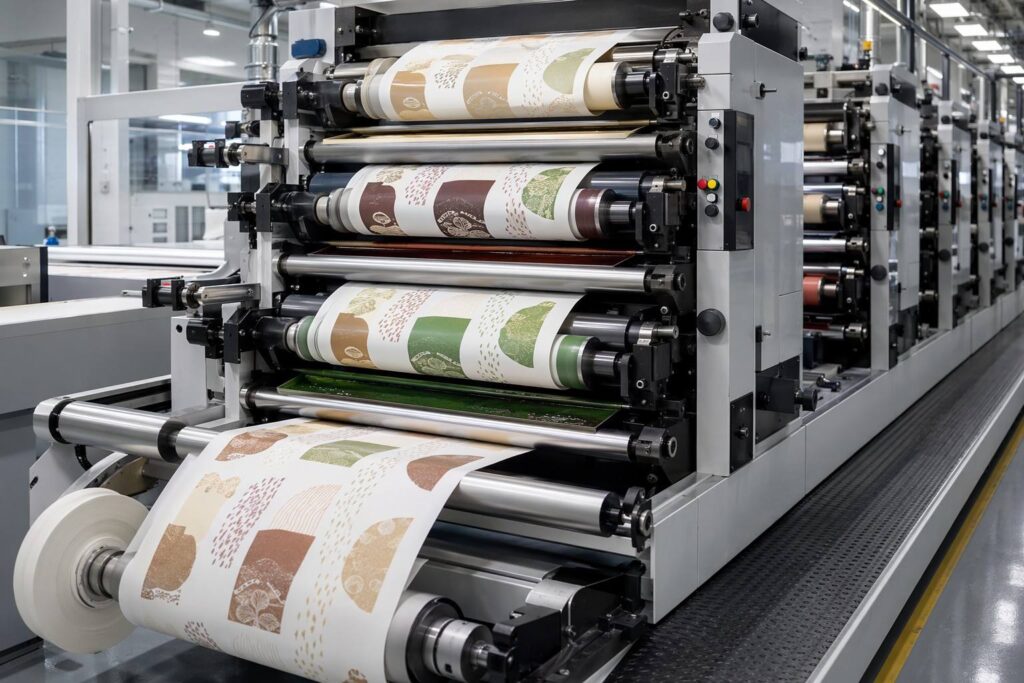
Step 2 – Printing

Customer artwork is printed using high-quality flexographic or offset printing equipment to achieve consistent colors, sharp graphics, and accurate brand reproduction.

Printing Process for Double Wall Paper Cups
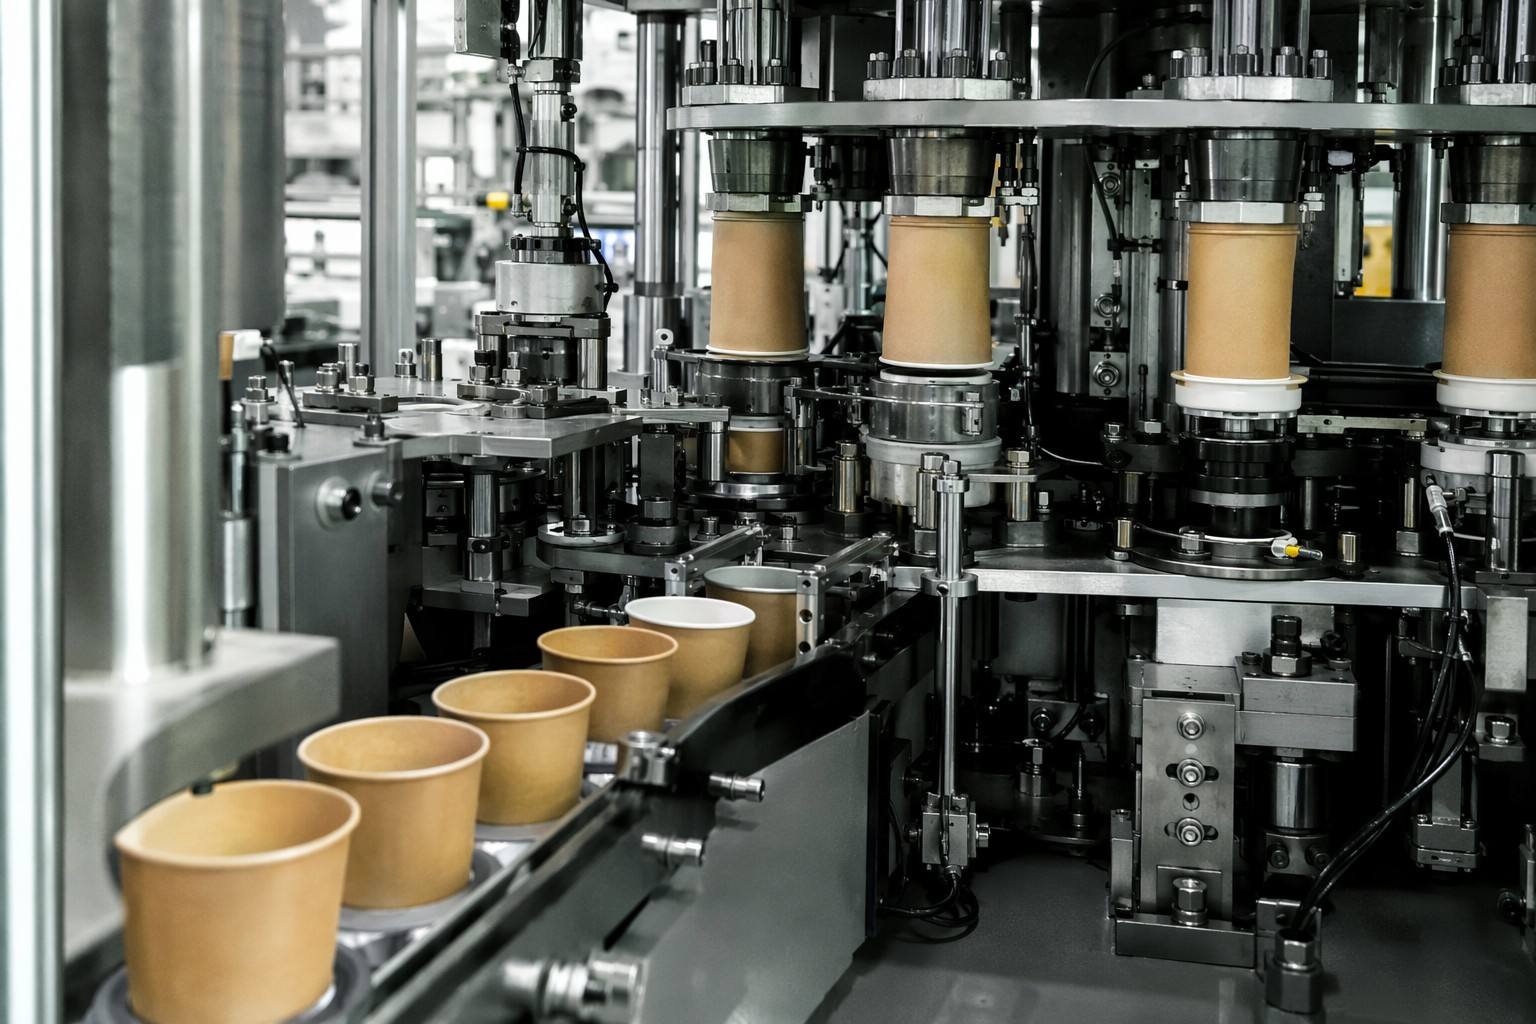
Paper Cup Forming Process

Step 3 – Cup Forming

The printed paperboard is formed into the inner cup body through automated forming equipment. Bottom sealing and side sealing are completed simultaneously to ensure reliable leak resistance.

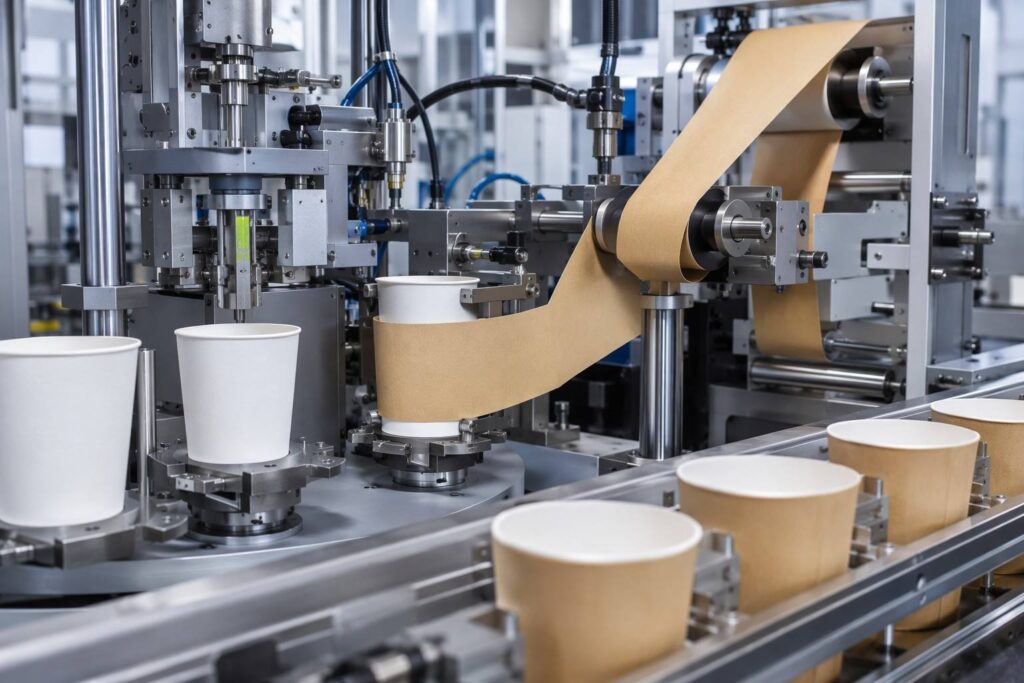
Step 4 – Outer Wall Wrapping

A second printed paper layer is accurately wrapped around the inner cup to create the insulating double wall structure.

This process determines the cup’s insulation performance, appearance, and structural strength.

Outer Wall Wrapping for Double Wall Paper Cups
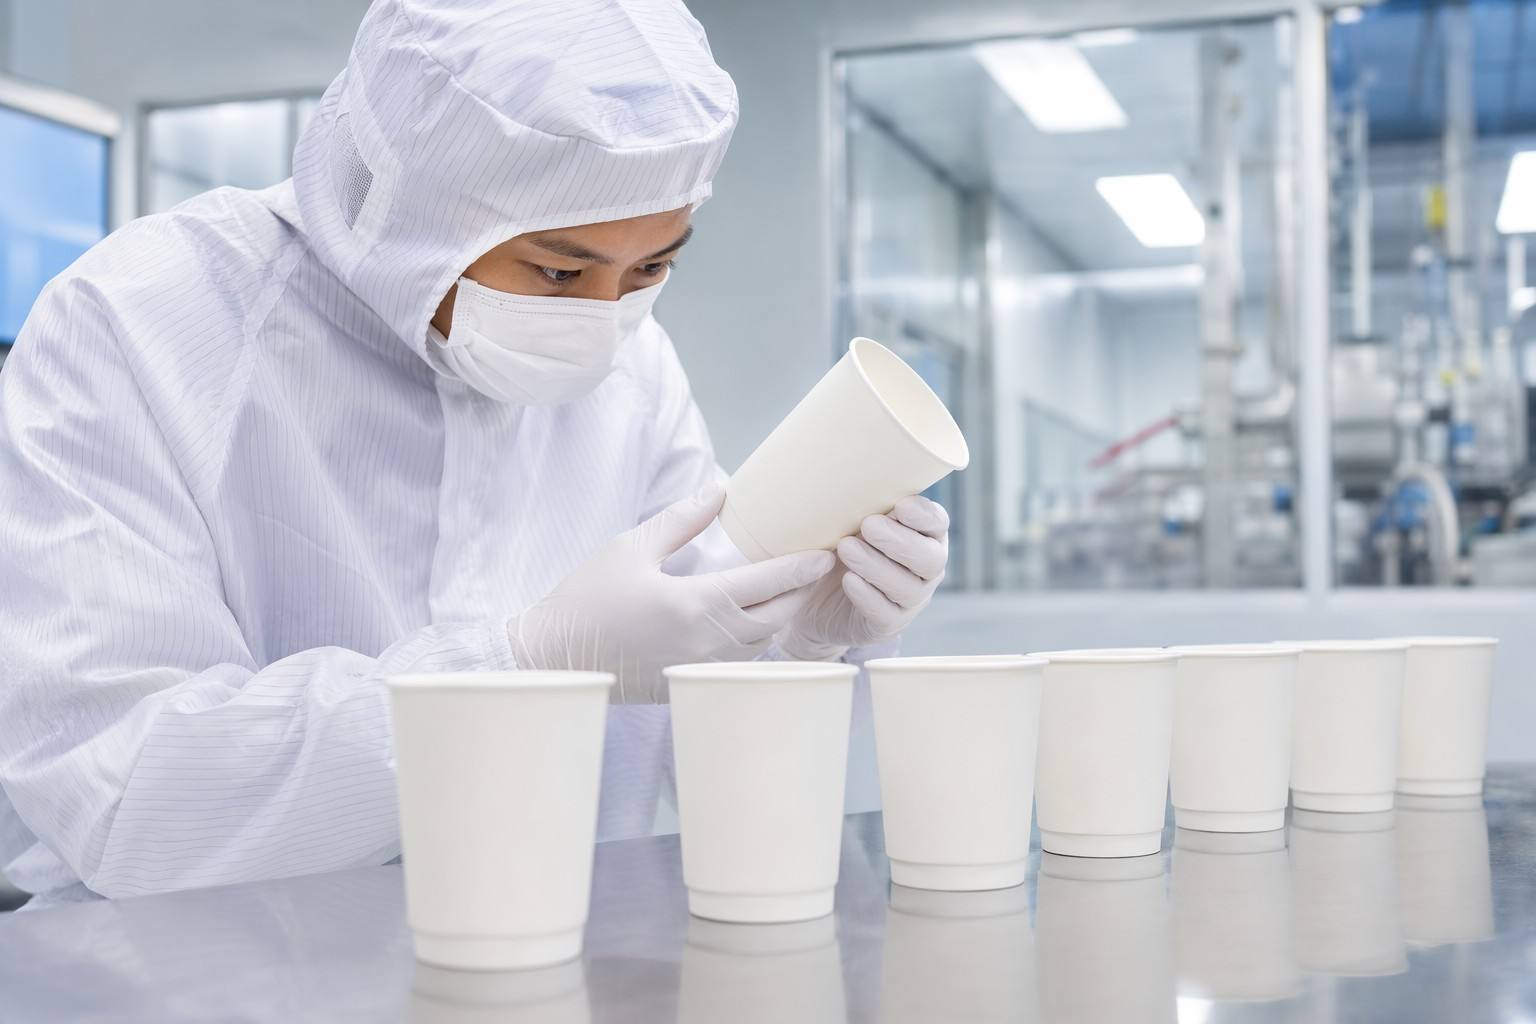
Quality Inspection of Double Wall Paper Cups

Step 5 – Inspection & Quality Control

Every production batch undergoes dimensional inspection, sealing tests, appearance verification, and random leak testing before packaging.

Quality control helps ensure consistent performance across large-volume production.

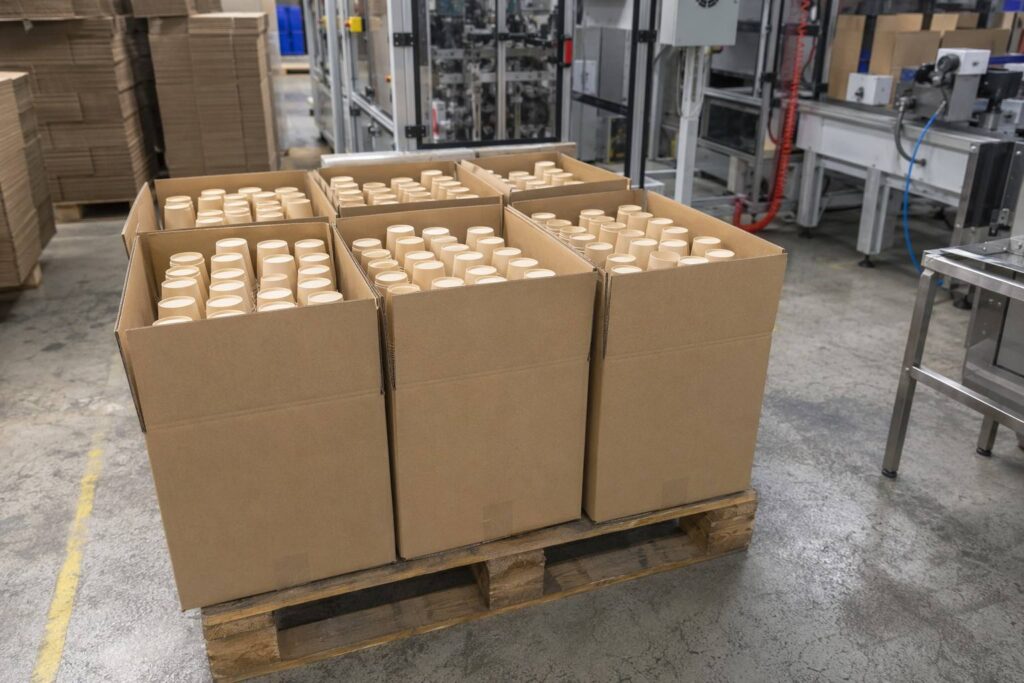
Step 6 – Packaging & Export

Finished products are automatically counted, packed into export cartons, palletized where required, and prepared for international shipment.

Packaging configurations can be customized according to customer requirements.

Packaging and Export of Double Wall Paper Cups

How to Choose the Right Double Wall Paper Cup Manufacturer?

Selecting the right manufacturing partner is just as important as selecting the right product. A reliable manufacturer not only delivers consistent product quality but also helps reduce procurement risks, improve supply chain stability, and support long-term business growth.

When evaluating potential suppliers, buyers should consider the following factors.


Manufacturing Experience

Choose a manufacturer with proven experience in producing disposable paper cups for international markets.

Experienced manufacturers are generally better equipped to manage product consistency, customization requirements, export documentation, and large-volume production.


Production Capacity

Evaluate whether the supplier has sufficient production capacity to support both your current purchasing volume and future business growth.

Consider factors such as:

  • Number of production lines
  • Monthly production capacity
  • Lead time stability
  • Peak season capacity

Stable production capability helps reduce supply interruptions and delivery delays.


Product Quality Management

Reliable manufacturers should implement standardized quality control procedures throughout the production process.

Typical inspections include:

  • Raw material inspection
  • Printing quality inspection
  • Dimension verification
  • Leak testing
  • Appearance inspection
  • Packaging inspection

A documented quality management system helps ensure consistent product performance across every shipment.


Customization Capability

Many beverage brands require packaging that reflects their visual identity.

Evaluate whether the manufacturer can support:

  • Custom logo printing
  • Pantone color matching
  • New artwork development
  • Custom cup sizes
  • Custom packaging
  • Private label production

Strong customization capability allows your packaging to become an effective brand communication tool.


Food Contact & Compliance Support

International markets often require different compliance documentation.

Before placing an order, confirm whether the supplier can provide support for:

  • Food-contact compliance
  • Factory audits
  • Material declarations
  • Product testing reports
  • Sustainability documentation

Preparing documentation early can significantly reduce project delays.


Export Experience

Manufacturers with extensive export experience are generally more familiar with international shipping requirements, packaging standards, and customer expectations.

Important considerations include:

  • Export packaging
  • Container loading optimization
  • International logistics coordination
  • Documentation preparation
  • Customer communication


Technical Support

A professional supplier should provide technical recommendations rather than simply accepting purchase orders.

Examples include:

  • Cup specification recommendations
  • Lid compatibility suggestions
  • Printing optimization
  • Material recommendations
  • Packaging optimization

Technical support helps buyers avoid unnecessary costs and improve overall project efficiency.


Customer Service

Timely communication is essential throughout every stage of a project.

Evaluate whether the supplier provides:

  • Dedicated account management
  • Fast quotation response
  • Sample support
  • Production updates
  • After-sales assistance

Reliable communication contributes to smoother project execution and long-term cooperation.


Pre-Purchasing Checklist for Buyers

Before placing an order for double wall paper cups, buyers are encouraged to review the following checklist to help ensure the selected products meet both commercial and technical requirements.

□ Cup Capacity

□ Cup Diameter & Height

□ Paperboard Specification

□ Coating Type (PE / PLA / Water-Based)

□ Printing Artwork Approval

□ Pantone Color Requirements

□ Lid Compatibility

□ Beverage Temperature Requirements

□ Food Contact Compliance

□ Sustainability Requirements

□ MOQ

□ Production Lead Time

□ Packaging Specifications

□ Carton Marking

□ Shipping Method

□ Destination Market Regulations

□ Annual Purchasing Forecast

□ Sample Approval

□ Factory Audit Requirements

□ Payment Terms

Completing this checklist before production begins can help minimize procurement risks and improve communication between buyers and suppliers.
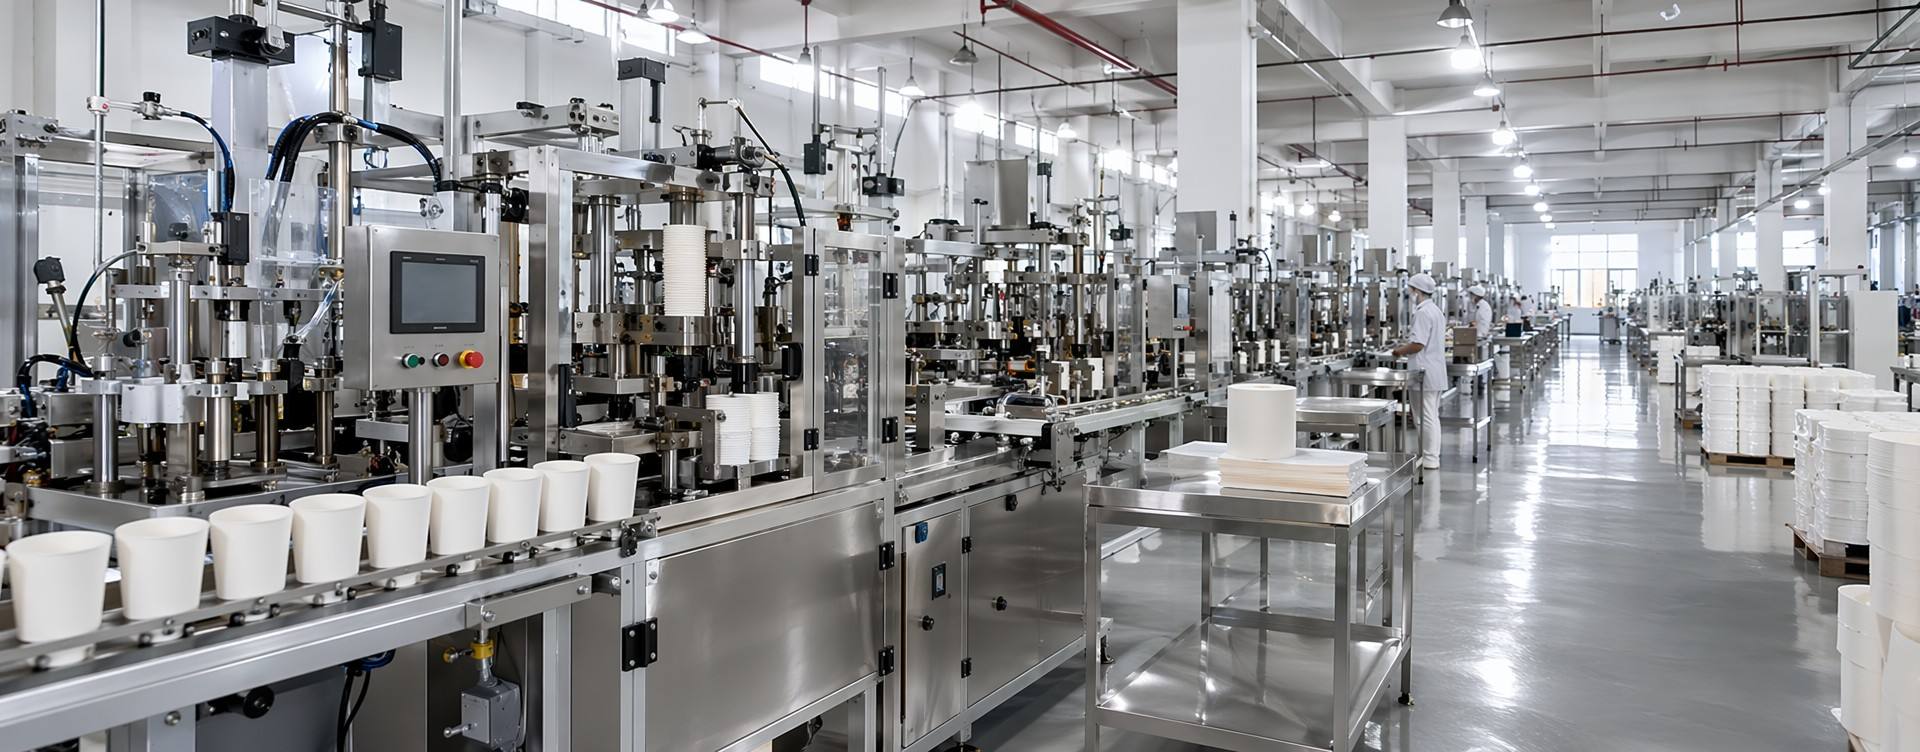
 

Choose DAILYECO to Be Your Professional Double Wall Paper Cup Manufacturer

DAILYECO Double Wall Paper Cup Manufacturing Facility


DAILYECO provides integrated disposable beverage packaging solutions for importers, distributors, coffee chains, hospitality groups, and global packaging brands.

As a manufacturing and supply chain partner, we focus on delivering stable quality, flexible customization, and reliable international supply for customers seeking long-term cooperation.


Factory Capability

DAILYECO Manufacturing Facility

Description

Employees

More than 1,000 employees

Production Lines

20 lines and 85 machines for paper cup production

Monthly Supply Capacity

50-55 40HQ containers

Cup Sizes

4oz–22oz standard molds available

Printing Capability

Flexographic & Offset Printing

OEM

Logo, printing, packaging, carton customization

ODM

Material, structure, artwork optimization

Technical Support

Available

Production MOQ

50,000pcs per size for common MOQ, ready goods or special MOQ based on specification and customization

Typical Lead Time

Approximately 30–35 days for new customized orders


Compliance & Documentation Support

DAILYECO can support customers with documentation according to destination market requirements.

Support may include:

  • Food-contact documentation
  • Factory audit support
  • Material declarations
  • Sustainability documentation
  • Product testing reports

View Our Compliance & Certification Support Page


Customization Services

DAILYECO support comprehensive customization throughout the product lifecycle, including:

  • Custom Logo Printing
  • CMYK & Pantone Printing
  • Custom Cup Structure
  • Private Label Solutions
  • Retail Packaging
  • E-commerce Packaging
  • Amazon Ready Packaging
  • Custom Carton Printing


Export Experience

DAILYECO products are exported to customers across North America, Europe, Australia, the Middle East, and many other international markets.

With extensive international shipping experience, we help customers simplify sourcing, reduce supply chain risks, and maintain stable long-term supply.


Customer Service

DAILYECO’s experienced international sales team provides responsive communication throughout the entire project lifecycle.

Support includes:

  • Product Consultation
  • Sample Arrangement
  • Artwork Confirmation
  • Production Updates
  • Shipping Coordination
  • After-sales Support


Continuous Product Development

As beverage packaging requirements continue to evolve, DAILYECO continuously develops new cup specifications, coating solutions, and customization capabilities to help customers respond to changing market demands.
REQUEST A QUOTE

Case Study

Case 1 European Coffee Chain Standardized Its Packaging Portfolio

Customer Background

A regional coffee chain in Europe was expanding from 28 stores to more than 60 locations. The company wanted to standardize its takeaway packaging while maintaining a premium customer experience across all stores.

Challenge

The customer had been using multiple cup suppliers with different cup dimensions, lid specifications, and printing quality. This resulted in inconsistent branding, higher inventory complexity, and frequent compatibility issues between cups and lids.

DAILYECO Solution

After reviewing the customer’s beverage menu and sales data, DAILYECO recommended simplifying the packaging portfolio to three standard cup sizes with unified lid specifications. We also optimized the artwork for large-scale flexographic printing to improve color consistency while maintaining production efficiency.

Results

The customer simplified inventory management, improved packaging consistency across all locations, and reduced the number of packaging SKUs required for daily operations. Standardized specifications also made purchasing and logistics more efficient as the business expanded.

Key Takeaways

Standardizing cup sizes and lid compatibility often delivers greater operational value than simply reducing unit price.


Case 2 Optimizing Packaging for a National Foodservice Distributor

Customer Background

A foodservice distributor supplying restaurants, hotels, and catering companies wanted to simplify purchasing while expanding its sustainable beverage packaging range.

Challenge

Managing numerous suppliers and inconsistent specifications increased purchasing complexity and warehouse management costs.

DAILYECO Solution

We consolidated multiple paper cup specifications into a standardized product range while coordinating compatible lids and complementary beverage packaging products.

Results

The distributor streamlined purchasing processes, simplified inventory planning, and created a more consistent product offering for downstream customers.

Key Takeaways

Consolidating product specifications often improves supply chain efficiency more effectively than continuously expanding product variety.


Case 3 Reducing Procurement Risks Through Early Technical Consultation

Customer Background

A beverage brand preparing for seasonal promotional campaigns required custom printed double wall paper cups with a strict delivery schedule.

Challenge

The project involved multiple stakeholders, customized artwork, and tight production timelines. Any design revision after production would have delayed the product launch.

DAILYECO Solution

Before production, our engineering and sales teams reviewed the artwork, paperboard specification, lid compatibility, packaging configuration, and logistics plan with the customer to identify potential risks in advance.

Results

The customer completed product approval before mass production, reducing unnecessary revisions and helping the project progress according to schedule.

Key Takeaways

Early technical communication often prevents costly production adjustments later in the project lifecycle.


FAQ 

What is the difference between a double wall paper cup and a single wall paper cup?

The main difference is insulation.

Single wall paper cups consist of one paper layer and often require an additional sleeve for hot drinks. Double wall paper cups incorporate a second paper layer, providing improved thermal insulation and eliminating the need for sleeves in many applications.


What is the difference between double wall and ripple wall paper cups?

Both designs improve insulation compared with single wall cups. Double wall paper cups provide a smooth outer surface that is ideal for premium printing, while ripple wall cups use a corrugated outer layer to maximize grip and thermal insulation.


What beverages are double wall paper cups suitable for?

They are widely used for:

  • Coffee
  • Tea
  • Cappuccino
  • Latte
  • Espresso
  • Hot Chocolate
  • Specialty Hot Drinks


Are double wall paper cups suitable for hot beverages?

Yes.

They are widely used for coffee, tea, cappuccino, latte, espresso, hot chocolate, and other hot beverages served in cafés, restaurants, hotels, offices, and takeaway businesses.


Do double wall paper cups keep drinks hotter for longer?

The double wall construction helps reduce heat loss while improving customer comfort. Although the cup itself is not a thermal flask, the insulating air layer helps maintain beverage temperature better than standard single wall paper cups.


Do I still need a paper sleeve?

In most situations, no.

The insulating double wall design usually provides sufficient protection for customers holding hot beverages. Some coffee brands may still choose sleeves for branding purposes.


What sizes are available?

Common capacities include:

  • 4 oz
  • 6 oz
  • 8 oz
  • 10 oz
  • 12 oz
  • 16 oz
  • 20 oz

Additional specifications may be available upon request.


Which lids are compatible?

Double wall paper cups can typically be matched with:

  • Paper lids
  • PP sip lids
  • PS lids
  • Flat lids
  • Dome lids

The most suitable lid depends on cup size and beverage application.


What coating options are available?

Typical coating options include:

  • PE coating
  • PLA coating
  • Water-based barrier coating

The most appropriate option depends on your target market, sustainability objectives, and local regulations.


Are double wall paper cups recyclable?

Recyclability depends on both the cup construction and the recycling infrastructure available in the destination market.

Buyers should evaluate local recycling capabilities before selecting coating materials.


Are compostable options available?

Depending on project requirements, PLA-coated or other sustainable coating solutions may be available for markets with industrial composting infrastructure.


Are these cups food safe?

Yes.

DAILYECO manufactures double wall paper cups using food-grade paperboard and supports food-contact compliance documentation according to customer requirements.


What is the MOQ?

We have a common MOQ 50,000 piece for one size, but minimum order quantities vary according to cup size, printing requirements, and customization level.

Our sales team can recommend the most suitable production solution based on your purchasing volume.


How long is the production lead time?

For new customized orders, a typical production lead time is approximately 30–35 days after artwork approval and order confirmation.


Which countries does DAILYECO export to?

Our products are supplied to customers across:

  • North America
  • Europe
  • Australia
  • Middle East
  • Asia
  • South America

Additional export destinations are supported according to customer requirements.


Can you provide samples before production?

Yes.

Samples are available for product evaluation, printing confirmation, and quality verification before mass production begins.


How should I choose between single wall, double wall, and ripple wall paper cups?

Selection depends on your business priorities.

  • Single wall paper cups are suitable for cost-sensitive projects.
  • Double wall paper cups provide an excellent balance between insulation, branding, and customer comfort.
  • Ripple wall paper cups offer maximum grip and insulation for premium takeaway coffee.


Which type of paper cup is best for my business?

The answer depends on your business model.

  • Coffee chains usually prefer double wall paper cups because of their premium appearance and branding opportunities.
  • Convenience stores often prioritize cost-effective standard paper cups.
  • Eco-focused brands may choose bagasse or PLA-based alternatives.
  • Hotels and hospitality groups generally prefer insulated cups that provide a better guest experience.

Selecting the right cup should consider customer experience, branding, sustainability goals, and operating costs rather than price alone.


Should I choose PE, PLA, or water-based barrier coating?

Each coating offers different advantages.

  • PE coatingis the most widely used solution for reliable performance and competitive pricing.
  • PLA coatingis suitable for markets requiring industrial compostable packaging.
  • Water-based barrier coatingsare increasingly selected in regions promoting recyclable fiber-based packaging.

The most appropriate choice depends on your destination market, applicable regulations, and sustainability strategy.


What information should I prepare before requesting a quotation?

Preparing complete project information helps suppliers recommend the most suitable product and provide accurate pricing.

Typical information includes:

  • Cup size
  • Annual purchasing volume
  • Printing requirements
  • Lid requirements
  • Target market
  • Packaging requirements
  • Delivery schedule

Providing these details early can significantly shorten quotation and sampling lead times.


How can I reduce overall packaging costs without sacrificing quality?

Many buyers focus only on unit price, but total packaging cost also depends on:

  • Appropriate cup specifications
  • Carton optimization
  • Container loading efficiency
  • Standard mold selection
  • Long-term purchasing plans

Working with an experienced manufacturer often reduces overall procurement costs more effectively than simply selecting the lowest-priced product.


Can DAILYECO develop custom printed paper cups?

Yes.

We provide complete OEM and private-label solutions, including:

  • Custom logo printing
  • Pantone color matching
  • Full-surface graphics
  • QR codes
  • Promotional artwork
  • Retail packaging
  • Carton customization


Can you help develop new cup sizes or special structures?

Yes.

For customers with unique packaging requirements, DAILYECO can evaluate custom tooling, structural optimization, and product development opportunities according to project volume and commercial feasibility.


How long does product development normally take?

For standard products with customized printing, production generally begins after artwork approval.

Projects involving new tooling or structural development require additional evaluation and development time depending on technical complexity.


Can DAILYECO support long-term supply programs?

Yes.

We work with distributors, coffee chains, hospitality groups, and packaging brands on long-term purchasing programs, providing stable production planning, quality consistency, and ongoing technical support.


Does DAILYECO only manufacture paper cups?

No.

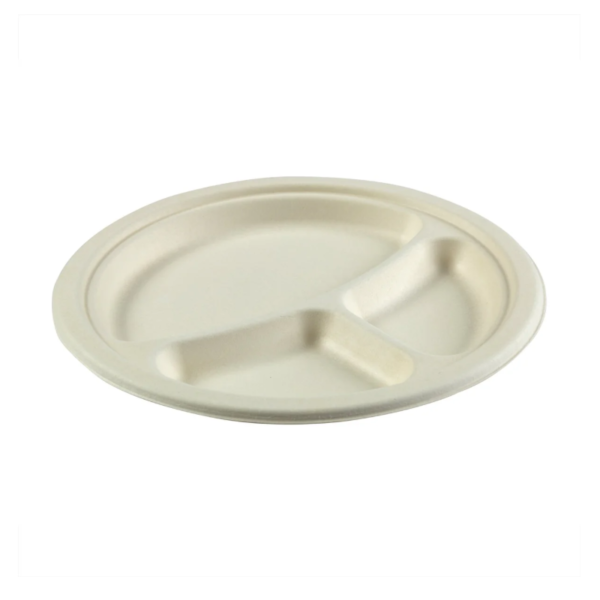
DAILYECO provides a comprehensive range of sustainable food packaging products, including paper cups, bagasse tableware, molded fiber packaging, paper food containers, cutlery, and customized packaging solutions, allowing customers to consolidate sourcing through a single manufacturing partner.


DAILYECO Industry Expert Tips: 10 Professional Insights for Sourcing Double Wall Paper Cups

Sourcing double wall paper cups is more than selecting a supplier or comparing quotations. Successful purchasing decisions require balancing product performance, brand presentation, regulatory compliance, supply chain stability, and total procurement cost.

Based on our experience supporting importers, distributors, coffee chains, and private-label brands worldwide, the following practical insights highlight some of the most common sourcing mistakes—and how to avoid them.

Common Mistake: Comparing Prices Without Comparing Specifications

Why It Matters

A quotation for a “12 oz Double Wall Paper Cup” does not necessarily describe the same product. Differences in paperboard grammage, coating type, cup dimensions, printing quality, and packaging configuration can all affect cost, performance, and customer experience.

DAILYECO Expert Advice

Request a detailed product specification sheet from every supplier before comparing prices.

Best Practice

Compare quotations only after confirming:

  • Cup dimensions
  • Paperboard specification
  • Coating type
  • Printing requirements
  • Packaging method
  • Lid compatibility


Common Mistake: Selecting Paperboard Based Only on Cost

Why It Matters

Using paperboard that is too light may reduce rigidity and insulation performance, while paperboard that is unnecessarily heavy increases material cost without delivering meaningful customer benefits.

DAILYECO Expert Advice

Choose paperboard according to beverage type, cup size, and customer expectations rather than simply selecting the heaviest or cheapest option.

Best Practice

Optimize paperboard specifications for each cup size to achieve the best balance between performance and cost.


Common Mistake: Choosing the Wrong Coating for Your Market

Why It Matters

Different countries have different packaging regulations, recycling systems, and sustainability expectations. A coating that works well in one market may not be the most suitable choice in another.

DAILYECO Expert Advice

Evaluate your destination market before selecting PE, PLA, or water-based barrier coatings.

Best Practice

Consider:

  • Local regulations
  • Recycling infrastructure
  • Composting availability
  • Brand sustainability goals
  • Consumer expectations


Common Mistake: Ignoring Cup and Lid Compatibility

Why It Matters

Leakage issues are often caused by poor compatibility between cups and lids rather than manufacturing defects.

DAILYECO Expert Advice

Always test the complete cup-and-lid combination before confirming production.

Best Practice

Perform practical testing using:

  • Hot beverages
  • Transportation simulations
  • Repeated opening and closing
  • Different filling levels


Common Mistake: Treating Printing as a Final Step

Why It Matters

For many coffee brands, the paper cup is one of the most visible customer touchpoints. Poor printing quality can reduce brand value even if the cup performs well.

DAILYECO Expert Advice

Review artwork with the same level of attention given to product specifications.

Best Practice

Confirm:

  • Pantone references
  • Artwork resolution
  • Logo positioning
  • Print coverage
  • Pre-production proofs

before mass production.


Common Mistake: Ordering Too Many Cup Sizes

Why It Matters

An excessive number of SKUs increases inventory costs, warehouse complexity, and purchasing management.

DAILYECO Expert Advice

Develop a standardized cup size strategy that covers the majority of beverage sales.

Best Practice

Many successful coffee businesses operate efficiently with only three primary sizes:

  • Small
  • Medium
  • Large

This approach also reduces the number of lid specifications that must be stocked.


Common Mistake: Evaluating Only Unit Price Instead of Total Procurement Cost

Why It Matters

The lowest unit price does not always produce the lowest operating cost.

Transportation efficiency, damage rates, inventory turnover, and production consistency all influence the overall cost of ownership.

DAILYECO Expert Advice

Evaluate suppliers using Total Cost of Ownership (TCO) rather than unit price alone.

Best Practice

Consider:

  • Product consistency
  • Lead time stability
  • Container loading efficiency
  • Packaging optimization
  • Customer complaint rates
  • Reorder efficiency


Common Mistake: Waiting Until Peak Season to Place Orders

Why It Matters

Demand for takeaway coffee cups often increases during colder seasons, promotional campaigns, and holiday periods. Late purchasing may result in extended lead times and higher logistics costs.

DAILYECO Expert Advice

Share quarterly or annual purchasing forecasts whenever possible.

Best Practice

Early production planning helps secure manufacturing capacity and improves delivery reliability.


Common Mistake: Choosing a Supplier Instead of a Long-Term Manufacturing Partner

Why It Matters

A supplier should provide more than products. Technical support, product development, and responsive communication become increasingly important as your business grows

DAILYECO Expert Advice

Evaluate whether the manufacturer can continue supporting your business over the next three to five years.

Best Practice

Assess suppliers based on:

  • Manufacturing capability
  • Product development
  • OEM experience
  • Export expertise
  • Customer service
  • Communication efficiency

—not simply quotation price.


Common Mistake: Asking Only for a Price Instead of Professional Advice

Why It Matters

Experienced manufacturers often identify opportunities to improve product performance or reduce costs before production begins.

DAILYECO Expert Advice

Treat your manufacturer as a technical consultant rather than only a production supplier.

Best Practice

Ask your supplier for recommendations on:

  • Cup structure optimization
  • Paperboard selection
  • Lid matching
  • Packaging configuration
  • Container loading
  • Cost optimization
  • Product standardization

Small technical improvements made before production often deliver significant long-term savings.


Final Recommendation

The most successful packaging projects are built on informed procurement decisions rather than simply choosing the lowest quotation.

By carefully evaluating technical specifications, market requirements, supply chain capability, branding objectives, and long-term cooperation potential, buyers can significantly reduce procurement risks while creating better customer experiences and stronger commercial value.

At DAILYECO, we believe our responsibility extends beyond manufacturing. Our goal is to help customers make better packaging decisions through practical technical guidance, transparent communication, and reliable long-term cooperation.


This Page Reviewed By

Lillian Guo

Food Packaging Compliance Manager

10+ Years of Experience

Specialized in:

  • Food Contact Compliance
  • Sustainable Packaging
  • Paper Cup Manufacturing
  • FDA
  • EU Food Contact Regulations
  • Packaging Compliance Documentation

Explore Our Related Sustainable Packaging

Discover more sustainable beverage and food packaging solutions from DAILYECO.

Contact Our Team

Looking for a reliable Double Wall Paper Cup Manufacturer?

Our packaging specialists are ready to support your project with:

✓ Product Catalog

✓ Free Product Consultation

✓ OEM & ODM Development

✓ Custom Printing Solutions

✓ Sample Requests

✓ Compliance Guidance

✓ Packaging Optimization

✓ Global Export Support

Whether you are sourcing for a coffee chain, distributor, importer, hospitality group, or private-label brand, our team will work with you to recommend the most suitable double wall paper cup solution for your business.

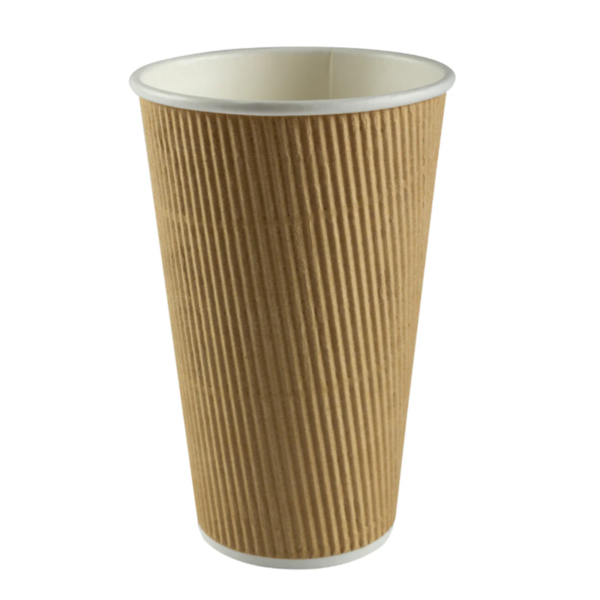
Submit Your Inquiry Now